産業用3Dプリンター:種類、造形可能体積、価格帯(2026年)
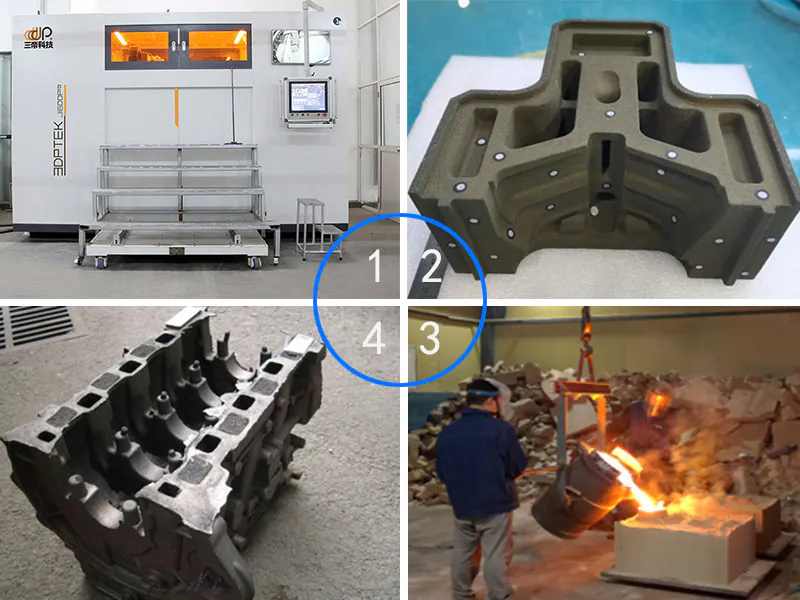
An industrial 3D printer is a production machine, specified by three things before frame size is mentioned: a build chamber that holds the part in one piece, unattended operation over weeks rather than hours, and a material system qualified for a structural alloy or foundry sand. Across the five families we build, build envelopes run from 160 × 65 × 65 mm on a benchtop metal binder-jetting system to 4,000 × 2,000 × 1,000 mm on a sand platform, with custom large-format lines to 10 m. 2026 price bands run from about US$120,000 to over US$1,000,000 ex-works.
This page is the entry point to the range: the five process families and where each one is used, what separates an industrial machine from a desktop unit, and the build volumes and price bands you can actually buy — then, for metal specifically, how binder jetting, SLM and gradient systems divide the work. It is written for foundries, casting buyers and manufacturing engineers specifying their first or third industrial system.
The five families of industrial 3D printer
They do not compete for the same part. The choice is driven by material, part size and annual volume — not by which machine is newest. Every family below is one we build and run in our own facilities, so the build volumes and bands are the ones we quote.
| 家族 | What it prints | Build volume (mm) | 2026 band, ex-works | Where it fits |
|---|---|---|---|---|
| Sand binder jetting | Sand molds and cores | 1,800 × 1,000 × 700 → 4,000 × 2,000 × 1,000 | ~US$218K – US$1.06M | Jobbing foundries replacing pattern tooling |
| SLS (sand and PSB wax) | Sand molds, cores and wax patterns | 500 × 500 × 500 → 1,050 × 1,050 × 650 | US$200K – US$1M+ | Wax patterns and mid-size molds |
| 金属バインダージェッティング | Sintered metal parts | 160 × 65 × 65 → 800 × 500 × 400 | US$120K – US$570K (metal range) | MIM replacement, batch parts |
| SLM | Fully dense metal parts | 120 × 120 × 150 → 300 × 300 × 250 | Inside the US$120K – US$570K metal band | Density-critical parts, gradient alloys |
| Large format and custom | Sand, metal and wax at scale | Up to 4,000 × 2,000 × 1,000; custom to 10 m | Quoted per line; J4000 sand ~US$682K – 740K | Oversized molds, one-piece parts |
Prices are 2026 ex-works bands and exclude the post-processing line — sintering furnace, depowdering and machining. The metal bands are broken down below; the per-part arithmetic for the other two families is in the sand printing cost そして SLS printer cost guides.
What separates an industrial machine from a small one
Four criteria separate the two categories, and only the first is about size.
- Build volume that clears the part. A production machine has to print a part in one piece, or the whole argument for additive disappears. Anything under roughly 100 mm in the largest axis is prototyping territory.
- Unattended operation. Industrial systems recover powder, monitor oxygen and log per-layer parameters without an operator present. A small unit stops when the operator goes home.
- Qualified material. The alloy must come with a data sheet, a powder supplier and a process window — not a resin cartridge.
- A post-processing route. The machine that prints the part is only half a cell. Every industrial metal system has a heat treatment, a depowdering step, a support removal step and a machining allowance behind it.
If a supplier answers the “is it industrial” question with laser wattage alone, the answer is incomplete. Wattage is cheap to print on a brochure; a qualified powder supply chain is not.
Metal 3D printers: three processes, three different economics
We build across three metal processes because they do not compete for the same part. Choosing between them is the first decision, and it is decided by geometry and volume rather than by preference.

Metal binder jetting — throughput per build
Metal binder jetting lays down a full powder bed and jets a binder across the entire layer at once. Because the deposition is parallel rather than serial, build rate scales with the print head, not the laser. That makes it the highest-throughput metal process per build cycle, and the one that makes sense when the same part number repeats.
The trade-off is density. Binder jet green parts require sintering, which means shrinkage to compensate, and the process holds roughly 97–99% density after sintering rather than the near-full density SLM reaches in one pass. For structural castings, manifolds, brackets and housings, that is usually acceptable; for a fracture-critical aerospace part, it is usually not.

Selective laser melting — density and tolerance
SLM melts each layer point by point with a laser, which is slower per unit volume but reaches near-full density in a single operation. It is the right process when the part needs a tight tolerance on an as-built surface, a thin wall, or a lattice that binder jetting would struggle to sinter without distortion.
Our single-laser entry system runs a 120 × 120 × 150 mm chamber; the largest rig in the range adds in-process machining on a 300 × 300 × 250 mm platform. The limiting factor on SLM throughput is rarely the laser itself — it is the support structures that have to be cut off, and the stress relief that has to follow.

Gradient and multi-material — the third category
Functionally graded metal parts sit outside both processes above. Rather than choosing one alloy, the deposit transitions between powders across the build so the finished part carries a hard surface on a tough core, or a wear-resistant face on a ductile body. It is still a niche, and it is a genuinely different capability rather than a marketing variant of SLM.

Build volume: what the seven systems actually print
Build volume is the number that decides whether a project is possible at all, so it is worth listing rather than describing. The table below covers every metal system in our current range. Overall dimensions matter as much as build volume — they determine the door the machine has to fit through and the floor space it has to stand on.
| モデル | プロセス | Build volume (mm) | Overall footprint (mm) | Positioned for |
|---|---|---|---|---|
| 3DPTEK J160R | 金属バインダージェッティング | 160 × 65 × 65 | 1,200 × 1,000 × 1,440 | Precision small parts and research |
| 3DPTEK J400P | 金属バインダージェッティング | 380 × 380 × 300 | 2,470 × 1,730 × 2,400 | Mid-scale production, ceramic capable |
| 3DPTEK J800P | 金属バインダージェッティング | 800 × 500 × 400 | 6,650 × 4,470 × 3,450 | Largest metal BJ platform, ceramic capable |
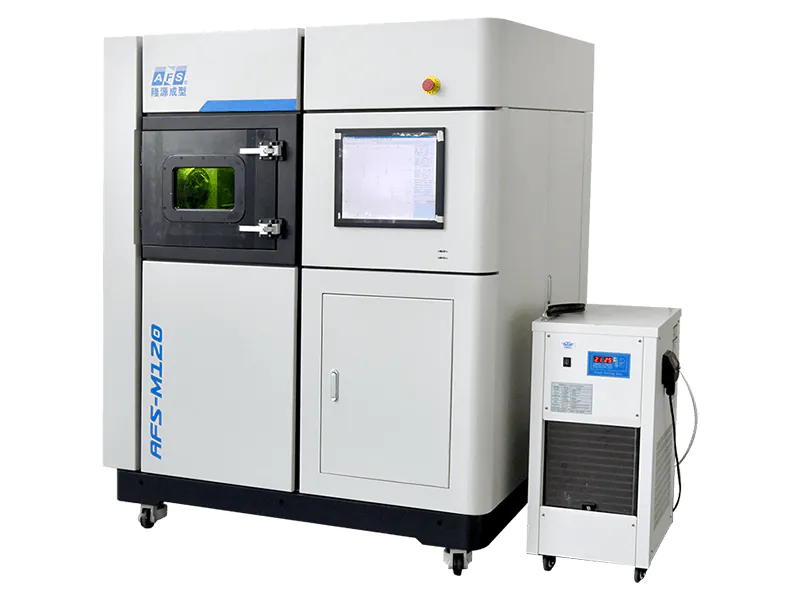
| AFS-M120 | SLM | 120 × 120 × 150 | 1,532 × 1,390 × 1,830 | Single-laser precision |
| AFS-M120X | SLM, dual material | 120 × 120 × 150 | 1,532 × 1,390 × 1,830 | Two-material gradient |
| AFS-M120XT | SLM, multi-axis gradient | 120 × 150 × 150 | 1,532 × 1,390 × 1,830 | Gradient along multiple vectors |
| AFS-M300XAS | SLM + in-process machining | 300 × 300 × 250 | 2,760 × 1,760 × 2,620 | Multi-material plus finished surfaces |
The widest practical gap is between the 120 mm SLM platform and the 800 mm binder-jetting bed. A part that fits the first will not fit the second without a redesign of its orientation, and a part designed for the second will waste most of the first. That is a specification decision, not a preference.
All seven models are listed with their full specifications on the metal 3D printer range page.
Throughput: the number that gets quoted and the number that decides
Vendors quote build rate in cubic centimetres per hour. It is a real number, but it is measured before post-processing, and post-processing is where most of the calendar time goes.
Binder jetting build rate
Because binder jetting deposits across the full layer, its build rate scales with the print head rather than the laser, and it is the process where the machine genuinely runs while nobody watches. A full bed of small brackets can be built in a single cycle; the same bed in SLM would take several times as long and require far more support.
The honest throughput figure for a binder jetting cell has to include sintering — a batch furnace cycle that is measured in days, not hours. Two machines that print at different speeds can finish the same job at the same time if one has to wait for a furnace slot.
SLM build rate and the post-processing tax
SLM throughput is dominated by three things that have nothing to do with laser power: the height of the part in the build direction, the amount of support structure, and the stress relief that follows. A part oriented to minimise support can be twice as fast as the same part oriented to minimise build height.
Our multi-material platform solves part of this differently — it machines the printed part to tolerance inside the same envelope, which removes a fixturing and re-datum step that would otherwise cost a day per batch.
What an industrial 3D printer costs
Across the five families the bands separate cleanly, and inside a family three things move the number: build envelope first, then process hardware — printheads or lasers — then automation. The metal bands are the most frequently quoted, so they are broken out here in detail.
Metal additive pricing is less mysterious than it looks once the bands are separated. There are three, and they are separated by process rather than by brand.
The three metal price bands
- Research and entry systems. Compact single-laser SLM platforms for small parts, dental and medical work, and process development.
- Production mid-range. Multi-laser or larger-bed binder jetting systems sized for a real part family and a real shift pattern.
- Large-format industrial. Systems where the build chamber is measured in hundreds of millimetres and the surrounding cell — powder handling, furnace, machining — is a capital project of its own.
Across the range we quote, entry-to-production metal systems land between US$120,000 and US$570,000 (approximately RMB 0.85 to 4.05 million ex-works), with the exact figure set by laser configuration, chamber size, powder handling and the post-processing line included. We deliberately do not publish a per-model price: the same platform configured for two different alloys and two different throughput targets is not the same machine.
What the machine price leaves out
The purchase price is the top of an iceberg. Below it sit four lines that catch first-time buyers:
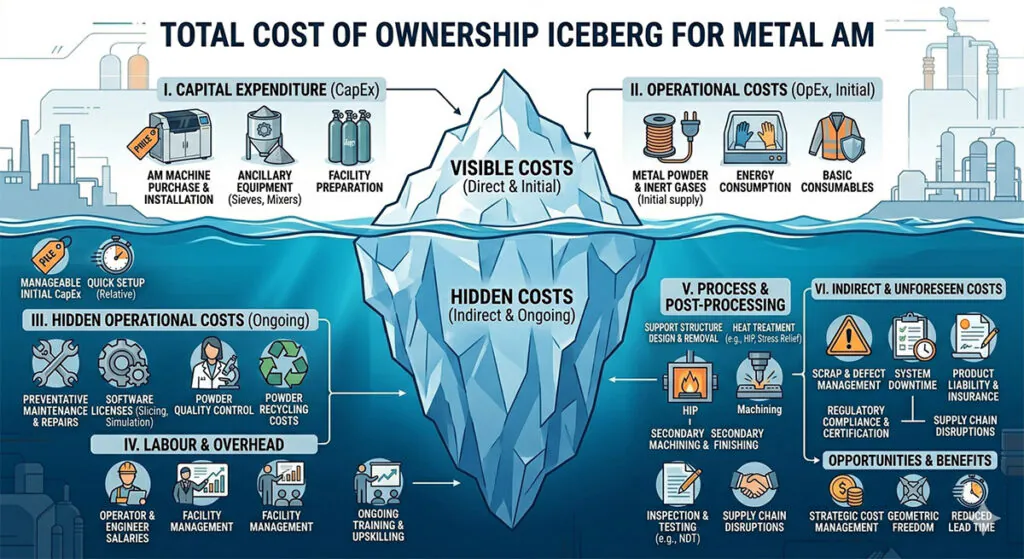
- Consumables. Metal powder is not a per-kilogram purchase so much as a per-batch one, and the usable fraction depends on the alloy and the reuse policy.
- Atmosphere and gas. Argon for SLM, and the oxygen monitoring that goes with it, is a recurring line rather than a one-off.
- Facility work. Floor loading, extraction, powder handling stations and — for binder jetting — a sintering furnace that can cost as much as the printer.
- Post-processing. Support removal, heat treatment, HIP where the application needs it, and machining allowances.
The full breakdown, with per-part cost arithmetic, is in our metal 3D printer cost guide. The short version: plan the whole cell before signing for the printer, not after.
Choosing by the part, not by the brochure
Every specification conversation reduces to four questions. Answering them in order removes most of the ambiguity.
| If the part… | The process that fits | なぜ |
|---|---|---|
| Fits inside 120 mm and needs a tight as-built tolerance | Single-laser SLM | Near-full density in one operation, minimal post-processing |
| Is small but needs two alloys in one body | Dual-material or multi-axis gradient SLM | The transition is built into the deposit, not assembled |
| Repeats at volume and tolerates 97–99% density | 金属バインダージェッティング | Throughput scales with head width, not laser speed |
| Is larger than 300 mm in two axes | Large-platform binder jetting | The only process in the range that clears the chamber |
| Needs a machined surface without re-fixturing | SLM with in-process machining | Print and finish in the same envelope |
The process comparison in more depth — including where each one loses on cost per part — is in metal binder jetting vs SLM and in what SLM can and cannot hold. If the question is which of two similar processes fits a casting workflow, this comparison works from the casting side rather than the machine side.
Where these systems already run
Every metal platform we sell is in production in one of our own five foundries before it is offered commercially. That matters for a specific reason: the failure modes that show up in year two — powder reuse drift, laser drift, furnace batch variance — are ones we have already met on our own floor rather than ones a customer discovers first.
Across the group that is more than 500 installations, 30+ qualified alloys and 45+ countries served since 1994, with ISO 9001 certification across the manufacturing centers.
よくある質問
産業用金属3Dプリンターとデスクトップ型金属プリンターの違いは何ですか?
造形容積、無人運転、認定済み材料。デスクトップ型の金属3Dプリンターは、固定式カートリッジから小型部品を造形しますが、産業用システムは認定済み合金を用いて、粉末を回収し、層ごとのデータを記録し、連続運転が可能になるよう設計されています。価格差は、フレームそのものよりも、材料システムや粉末処理の仕組みに大きく起因しています。.
1台の機械で、鋼とアルミニウムの両方を印刷することは可能ですか?
SLMについては可能です。ただし、合金ごとに粉末を交換し、検証済みのプロセスウィンドウを設定する必要があります。バインダージェッティングでは、ステンレス鋼、工具鋼、セラミック粉末に対応しています。制約となるのは装置そのものではなく、粉末の取り扱いおよび合金間の交差汚染の管理です。.
ビルドにはどれくらい時間がかかりますか?
これは、部品の複雑さよりも、造形高やサポートの体積に大きく左右されます。 高さ150 mmのSLM造形は、冷却時間を含めて通常1~3日かかります。一方、バインダージェッティングのベッド全体を造形する場合は、印刷に数時間かかり、その後、数日にわたる炉内処理サイクルが必要です。当社では、1回の造形にかかる時間ではなく、1週間あたりの造形回数で見積もりを提示しています。これは、生産計画担当者が使用する数値だからです。.
産業用金属3Dプリンターの価格はいくらですか?
Entry-to-production systems run from US$120,000 to US$570,000 (approximately RMB 0.85 to 4.05 million ex-works), depending on process, chamber size, laser configuration and the post-processing line included. Large-format and multi-material configurations sit at the top of that band. The machine is roughly half the total cell cost; the 費用ガイド breaks down the rest.
Do I need a furnace as well as the printer?
For binder jetting, yes — sintering is part of the process, not an optional extra, and the furnace is a capital line item in its own right. For SLM, a stress-relief furnace is still required but at a smaller scale. Neither is included in a printer quotation unless it is written into the line items.
What is an industrial 3D printer?
A production additive manufacturing system specified by build volume, unattended operation and a qualified material system — not by frame size. Industrial machines print foundry sand molds, wax patterns or metal parts at build volumes from 160 mm to 4,000 mm, and are bought with a post-processing route (sintering furnace, depowdering, machining) rather than as a standalone box.
How much does an industrial 3D printer cost?
2026 ex-works bands by family: sand binder jetting about US$218,000–1,060,000; SLS for sand and PSB wax US$200,000–1,000,000+; metal binder jetting and SLM US$120,000–570,000; large-format and custom lines are quoted per build envelope, with the J4000 sand platform at about US$682,000–740,000. Post-processing sits outside those figures.
Which industrial 3D printing process should I choose?
Match the process to the material and the part. Binder jetting for sand molds and cores, or metal green parts at volume; SLS for sand molds and PSB wax patterns; SLM when the part must be fully dense or needs gradient alloys; large-format platforms when the part exceeds a standard chamber. The part-fit table above maps four common cases.
関連記事
If the process question is still open, SLS vs SLM separates the two laser routes and metal binder jetting vs SLM covers the metal routes. The metal 3D printer cost guide carries the per-part arithmetic, the sand そして SLS guides cover the other two families, and the range overview lists every model with its build volume. If you would rather print parts than buy a machine, start with the 金属3Dプリントサービス. The 金属3Dプリンターガイド is the metal-only version of this page: routes, materials and 2026 price bands without the other four families.
Ready to specify a system?
Send the part drawing, the annual volume and the alloy. We will come back with the process that fits, the build volume it needs, the cell around it and a quotation that separates the machine from the post-processing line. If the part is better served by printing it through our 金属3Dプリントサービス before committing to a purchase, we will say so.
Request an industrial system proposal →