
3D Printer That Prints Metal: Binder Jetting vs SLM, Materials and Price Bands (2026)
A 3D printer that prints metal is a production machine, not a desktop unit: it either jets binder into a metal powder bed and sinters the green part, or melts each layer with a laser. We build both routes on one open material platform — 7 systems, 30+ qualified alloys, build volumes from 160 × 65 × 65 mm to 800 × 500 × 400 mm, and 2026 ex-works prices from about US$120,000 to US$570,000.


What a metal 3D printer actually does
Every metal 3D printer does the same three things: spreads a thin layer of metal powder, places material only where the part is, and repeats until the build is finished. Where machines differ is how they place the material — and that decides density, speed, materials and cost per part.
Binder jetting prints the whole layer at once with an inkjet head, then sinters the green part in a furnace. SLM (selective laser melting) melts the layer point by point with a 500 W fibre laser, producing a fully dense part straight off the plate. A third option, gradient SLM, blends two to four powders in one build.
The difference is not cosmetic. A binder-jetted green part leaves the machine at roughly 67% density — the furnace is what makes it metal. An SLM part leaves the machine at 99.9% relative density but has to be cut off its supports.
- Green part + sintering — highest throughput per build, 3–5× lower cost per part at volume than SLM.
- Laser melting — 99.9% relative density, wrought-equivalent properties, supports required.
- Gradient / multi-material — 2–4+ alloys in one continuous build.
The two production routes, side by side
| What matters | Metal binder jetting | SLM (selective laser melting) |
|---|---|---|
| How it forms | Printhead deposits binder across the full powder bed; the green part is debinded and sintered in a furnace. | 500 W IPG fibre laser fully melts each layer, point by point. |
| Density | Green density ~67%, driven to 97–99% in the sintering furnace; shrinkage compensated in the model. | 99.9% relative density straight off the plate; wrought-equivalent mechanical properties. |
| Throughput | Up to 8 L/h metal and 12 L/h silicon carbide on the J800P. | Layer-by-layer; 6 m/s scan speed; faster to a finished part. |
| Supports | None — the powder bed supports every overhang, so nobody cuts supports off. | Required and removed afterwards. |
| Accuracy | ±0.1 mm; 1200 dpi printhead resolution. | ±0.1 mm per 100 mm. |
| Materials | Stainless steel, tool steel, copper and tungsten alloys, silicon carbide; alloy-specific sintering profile. | Stainless steel, tool steel, aluminium, titanium, cobalt-chrome, nickel superalloys. |
| Post-processing | Depowder, debind, sinter, optional machining; the furnace is a capital line item. | Stress relief, support removal, machining. |
| Cost per part at volume | 3–5× lower than SLM — the reason MIM lines switch. | Higher per part; wins when density or gradient geometry decides. |
Which route fits the part
Four questions settle it before any quotation: how big is the part, what density does it need, how many per month, and which alloys are involved.
| If the part… | The route that fits | Why |
|---|---|---|
| Fits inside 120 mm and needs a tight as-built tolerance | Single-laser SLM | Near-full density in one operation, minimal post-processing. |
| Is small but needs two alloys in one body | Gradient SLM | Dual-powder feeding; 100+ compositions in a single build. |
| Exceeds 120 mm and volume decides the business case | Metal binder jetting | Throughput per build; the sintering furnace is part of the plan. |
| Replaces a MIM line or a machining route | Metal binder jetting | Green part + sinter mirrors MIM; no tooling, no supports. |
| Has fine internal channels or thin walls | SLM | Resolution and density in one pass; supports do the overhangs. |
Build volumes: the seven metal systems
Seven platforms, two routes, one open material platform. The build envelope is the first number that decides which machine fits — the second is throughput after post-processing.

- Build volume
- 160 × 65 × 65 mm
- Throughput
- 400–1200 dpi · 165 cc/h

- Build volume
- 380 × 380 × 300 mm
- Throughput
- 3 or 6 heads · 3.6 L/h
- Build volume
- 800 × 500 × 400 mm
- Throughput
- 8 L/h metal / 12 L/h SiC

- Build volume
- 120 × 120 × 150 mm
- Laser
- 500 W IPG fibre

- Build volume
- 120 × 120 × 150 mm
- Compositions
- 100+ per build

- Build volume
- 120 × 150 × 150 mm
- Gradient
- X + Z · 3+ powders

- Build volume
- 300 × 300 × 250 mm
- Laser
- 2 × 500 W · in-process CNC
Materials: the grades behind the 30+ alloys
The platform is open: certified third-party powder is fine as long as it meets the published parameter set, and full parameter sets — layer thickness, laser or binder settings, debind and sinter recipes — ship with each qualified material.
| Family | Qualified grades |
|---|---|
| Stainless steel | 304, 316L, 17-4PH |
| Titanium | Ti6Al4V |
| Tool steel | H13, 4140, 2709 |
| Cobalt-chrome | CoCrMo |
| Nickel superalloy | Inconel 625, 718 |
| Aluminium | Al alloys |
| Copper & tungsten | Cu, W alloys |
| Ceramic (BJ only) | Silicon carbide |

Gradient metal: two alloys, one monolithic part
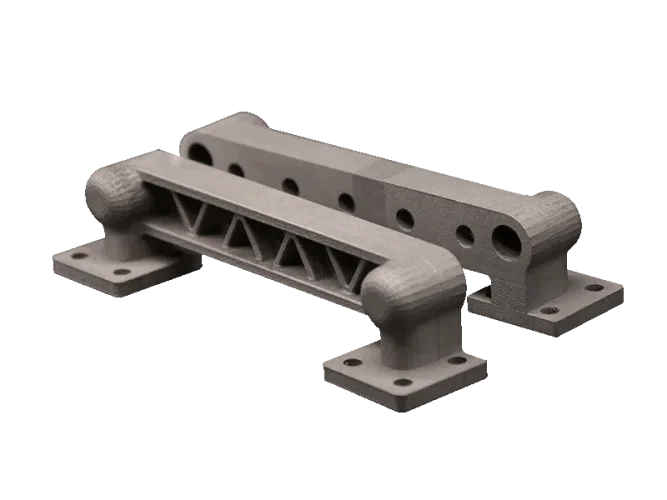
Traditional manufacturing welds, brazes or fastens dissimilar metals — which creates the weak point. Gradient SLM builds the transition atom by atom, so hardness, wear resistance and corrosion resistance can change across the same part.
2709 tool steel + 316L
A hard mould face with corrosion-resistant cooling channels behind it, built in one piece. No welds, no joints — properties designed layer by layer.

316L + CoCrMo
Corrosion-resistant stainless transitions into high-wear cobalt-chrome — biomedical and marine parts that used to be two pieces joined together.

100+ compositions
The M120X dual-powder head prints 100+ alloy compositions in one build; the M300XAS prints the gradient part and machines it without re-fixturing.
What a metal 3D printer costs in 2026
Entry-to-production metal systems run from US$120,000 to US$570,000 ex-works (approximately RMB 0.85–4.05 million), depending on process, build envelope, laser or printhead count, and gradient capability. Two machines with the same frame can be different products once materials and throughput targets change.
| Band | What sits in it | What moves the number |
|---|---|---|
| Entry | Compact single-laser SLM (AFS-M120 family) | Laser power, build envelope, powder handling |
| Production mid-range | Binder jetting sized for a real part family (J400P) | Printhead count, automation, material qualification |
| Large-format | J800P binder jetting, AFS-M300XAS hybrid SLM | Build envelope, laser count, in-process machining |
Where the money actually goes
| Cost driver | Binder jetting | SLM |
|---|---|---|
| Machine time | Printing at inkjet speed; cost per part falls as the tray fills | Laser time dominates; nesting helps less |
| Powder | Metal powder plus binder (15% binder vs 40–50% in MIM feedstock) | Powder with recycling; alloy cost is a real line item |
| Furnace | Debind and sinter batch; cost per part depends on furnace fill | Stress relief, smaller scale |
| Supports | None | Removal labour and stock allowance |
| Machining | Near-net; critical faces machined | More stock for supports, more machining |
| Inspection | Density and tensile per lot | Density and tensile per lot |
Outside the machine price: the sintering furnace binder jetting needs (quoted separately), depowdering, stress relief, machining, powder handling and installation. Budget the cell, not the box.
Design rules that decide success
Metal parts are not redesigns of plastic parts. These rules decide whether a part prints well, sinters straight and machines economically.
Design for the furnace (binder jetting)
- Build the shrinkage allowance into the model — the green part is ~67% dense and shrinks during sintering.
- Keep wall sections uniform; isolated masses and thin-to-thick transitions are where sinter distortion starts.
- Internal channels need no support, but they do need a way for binder and loose powder to escape before sintering.
- Leave critical faces with machining stock; ±0.1 mm is the process accuracy, not a machining tolerance.
Design for the plate (SLM)
- Every overhang needs support: orient the part to minimise it, then plan the removal.
- Closed channels need drain holes so trapped powder can leave.
- ±0.1 mm per 100 mm is the as-built accuracy; threads, bores and sealing faces are cut afterwards.
- Stress relief is part of the process — thin, long parts distort without it.

Metal 3D printing vs casting — and the other metal AM routes
Printing and casting are not competing for the same order. The choice is decided by tooling, lead time and complexity — and by annual volume.
| Metal 3D printing | Casting | |
|---|---|---|
| Tooling | None | Pattern and mould; $5,000–150,000+ |
| Lead time | Days | Weeks to months |
| Complexity | Conformal channels, thin walls, lattice | Limited by cores and draft angles |
| Volume | Low to mid; batch parts with binder jetting | High volume, simple geometry |
| Best fit | Complex, low-volume, design iteration | Repeat orders with stable geometry |

When volume is high but the geometry is still complex, the middle path is to print the sand mould or the wax pattern instead — sand 3D printers and wax 3D printers.
Other metal AM routes you will be quoted
Bound metal deposition extrudes a metal-filled filament or rod and sinters it — the same furnace logic as binder jetting, at a smaller scale and lower throughput. Metal FDM prints a metal-polymer composite; it is useful for prototypes and fixtures, not for structural parts. EBM (electron beam melting) melts in a vacuum and suits titanium, at a coarser resolution. None of them change the decision above: if the part needs full density in titanium or a superalloy, it is a melting route; if it needs volume economics in steel, it is binder jetting.
Quality: what to specify before the first build
Density
Green parts leave the printer at ~67% density; sintering brings them to 97–99%. Specify the density method — Archimedes or CT — and the acceptance threshold, not just “fully dense”.
Mechanical properties
Tensile bars printed with the lot, tested per build or per lot. Heat treatment — stress relief, solution and age for titanium and aluminium — is specified with the part, not after the fact.
HIP and machining
Hot isostatic pressing closes residual porosity for critical parts; machining removes supports, cuts threads and bores and holds the tolerances the process cannot. Both are line items, not surprises.
For aerospace and medical parts, the certificate matters as much as the density: material cert, build record and inspection report travel with the lot.
What these machines are used for

Replace injection-moulding tooling
At 15% binder instead of 40–50%, debind is faster and the furnace cycle is shorter. Tool-less production means a design change costs a re-slice, not a new mould — and at volume the cost per part is 3–5× lower than SLM.
Titanium and superalloys
Ti6Al4V and Inconel 625/718 parts where strength-to-weight and certified density matter more than unit cost — brackets, housings, implants and hot-section components.
Functionally graded materials
Two to four alloys in one continuous build, 100+ compositions on the M120X, X and Z control on the M120XT — for materials research and parts that used to be assemblies.
Conformal cooling and gradient wear faces
Cooling channels a drill cannot reach, plus a hard tool-steel face with a corrosion-resistant core in one build. The mould runs cooler and cycles faster.
Five questions that pick the machine
Work down this list with your own part in hand. Most buyers have the answer by the third question.
How big is the part?
Under 120 mm in X and Y points at the AFS-M120 family. Up to 380 mm points at the J400P. Past 500 mm you are in J800P territory at 800 × 500 × 400 mm — and if the part is larger than any build box, it is a design problem, not a machine problem.
Does it need full density as-built?
If it must be fully dense the moment it leaves the machine, or the alloy is titanium or a superalloy, you need SLM. Binder jetting reaches density in the furnace, not in the machine.
How many parts per month?
Volume decides between binder jetting and SLM more often than geometry does. At volume, the tray-fill economics of binder jetting win; at low volume, SLM avoids the furnace and the sinter batch.
Does it need two alloys?
If the part needs a hard face and a tough core, or a wear surface on a corrosion-resistant body, gradient SLM gives it in one build instead of a weld or a braze.
Buying a machine, or buying parts?
If volume does not justify capital yet, do not buy — run the parts through our metal 3D printing service first and get a free feasibility review on the drawing.
What does the post-processing line add?
Furnace, depowdering, stress relief, machining and inspection are part of the cell. Budget them before comparing two machine quotations.
Frequently asked questions
What is a 3D printer that prints metal?
A production additive manufacturing machine that builds metal parts layer by layer from powder. It either jets a binder into a metal powder bed and sinters the green part, or melts each layer with a laser. Both routes print parts that are impossible or uneconomic to machine or cast — conformal cooling channels, thin walls, consolidated assemblies.
How much does a metal 3D printer cost?
Entry-to-production systems run from US$120,000 to US$570,000 ex-works depending on process, build envelope and laser or printhead count. Binder jetting needs a sintering furnace as a separate capital line item; SLM needs stress relief at a smaller scale. Neither is included in a printer quotation unless it is written into the line items.
Can one machine print both steel and aluminium?
Yes for SLM, with a powder change and a validated process window per alloy. Binder jetting is more alloy-specific: the sintering profile is tuned to the alloy, so switching families is a process-qualification exercise rather than a material swap.
Can binder jetting produce fully dense parts?
After sintering, yes — 97–99% relative density in production, with shrinkage compensated in the model. The part leaves the printer at about 67% density; the furnace is what makes it metal, which is why the furnace is part of the capital plan.
What tolerance can I expect?
±0.1 mm process accuracy on binder jetting and ±0.1 mm per 100 mm on SLM. Anything tighter — bores, threads, sealing faces — is machined after the build, and the design should leave stock there.
Do I need a furnace as well as the printer?
For binder jetting, yes — sintering is part of the process. For SLM, a stress-relief furnace is still required but at a smaller scale.
How long does a build take?
It depends on build height and support volume more than part complexity. A 150 mm tall SLM build typically runs one to three days including cool-down; a full binder jetting bed runs hours to print and then a furnace cycle measured in days.
What is the difference between metal 3D printing and casting?
Printing needs no pattern or mould, so lead time drops from weeks to days and design iteration is cheap. Casting wins on repeat volume with stable geometry. Many foundries run both: print the complex or low-volume parts, cast the repeat orders.
Is the material platform open?
Yes. We publish the process parameters, and certified third-party powder is acceptable as long as it meets the published specification. 30+ alloys are qualified, and additional materials can usually be qualified on request.
Can I print a part before buying a machine?
Yes — the metal 3D printing service covers materials, tolerances and inspection, with a free feasibility review on the drawing. It is also the honest answer when volume does not yet justify capital.
Send the part, get the route
Send the drawing, the annual volume and the alloy. We come back with the process that fits, the build volume it needs, and a quotation that separates the machine from the post-processing line. If the part is better printed through our service before committing to a purchase, we will say so.
Request a quote