
Stainless Steel Casting Without Tooling Cost
A pattern is the most expensive and slowest part of any stainless steel casting project. We remove it. Printed sand moulds and printed wax patterns go straight from your CAD file to the foundry floor, so a design change costs nothing and the first part can be poured while a conventional shop is still quoting pattern work.
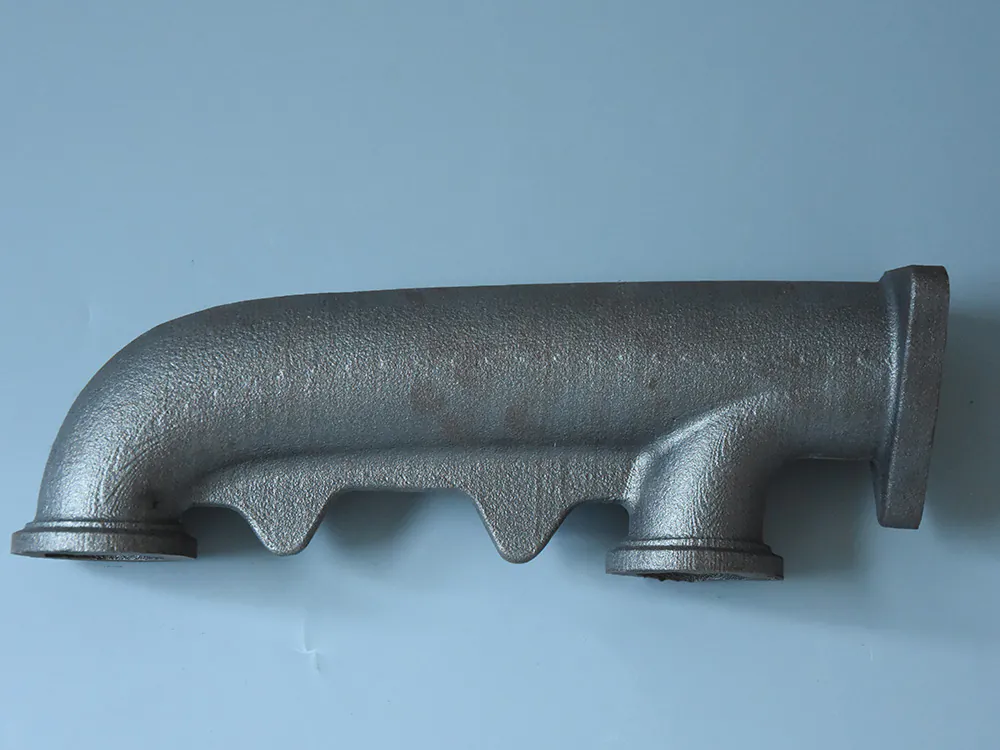
- 1 tMaximum single cast weight
- 1.5 mMaximum casting dimension
- 20 joursTypical small-batch delivery
- CT8 to CT9Standard dimensional tolerance
Stainless grades we cast
Stainless sits inside our cast steel line, which we run through shell casting and investment casting. The three grades below cover most enquiries; duplex and the high-temperature alloys come up in pumps, valves and process equipment.
304 and 304L
The general-purpose austenitic grade. Food and beverage equipment, architectural hardware, general industrial parts. Good weldability and dependable corrosion resistance across a wide temperature range.
316 and 316L
Molybdenum gives it resistance to pitting and crevice corrosion that 304 does not have. This is the grade for chlorides, saltwater, chemical process lines, pumps and valve bodies.
17-4PH
Precipitation-hardening martensitic stainless. It reaches high strength and hardness after heat treatment, so it suits shafts, valve stems and fittings where 304 or 316 would be too soft.
Duplex and superalloys
Duplex stainless for chloride service where 316 stress-cracking is a risk. Beyond stainless, we cast nickel and cobalt superalloys, including Inconel 718 and Hastelloy, for high-temperature parts.
| Grade | What it gives you | Where it breaks down |
|---|---|---|
| 304 / 304L | Cheapest of the austenitic grades, easy to weld and form, good across a wide temperature range | Chlorides. It pits and crevice-corrodes in saltwater and chemical service |
| 316 / 316L | Molybdenum resists pitting and crevice corrosion, so it holds up in chlorides and acids | Chloride stress corrosion cracking at elevated temperature and tensile load |
| 17-4PH | High strength and hardness after precipitation hardening, with moderate corrosion resistance | Not a substitute for 316 in aggressive chemical service; corrosion resistance is a step down |
| Duplex | Roughly double the yield strength of 316 plus resistance to chloride stress cracking | Higher alloy cost, and welding needs tighter control than the austenitic grades |
For the underlying material data across sands, binders, metal powders and wax, see our foundry materials guide.
How a stainless part moves through the works
Two routes leave the same CAD file and converge at the finished part. One prints a sand mould and core, the other prints a wax pattern and builds a ceramic shell. Both skip pattern making, which is where the schedule usually goes — and because the mould is data rather than hardware, a revision between the first and second part costs a reprint rather than a new pattern.

Cores printed in one pieceNo joint line to clean up 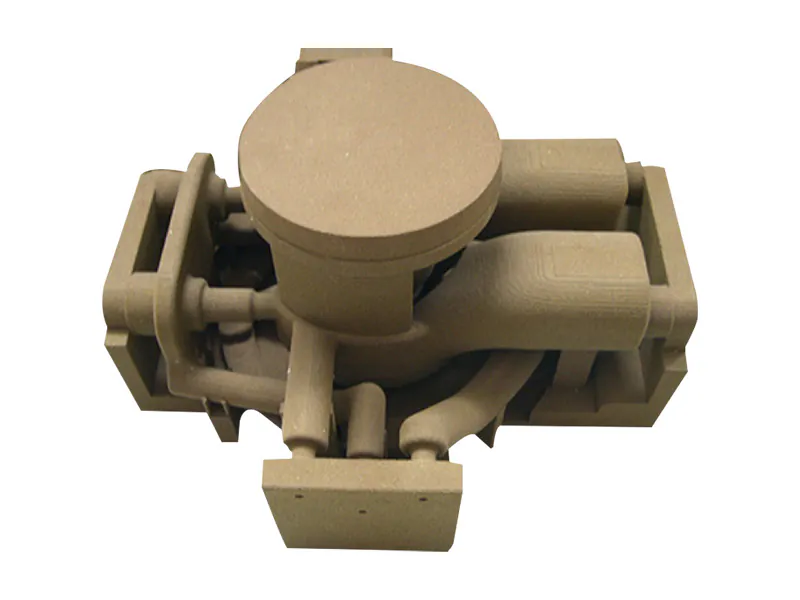
Mould for a pump valve bodyPrinted directly from CAD
The two production routes we run for stainless. Route choice is decided by wall thickness and internal detail, not by the alloy.
Two routes from CAD to a stainless part
Which one fits depends on geometry and how much detail the part carries, not on the alloy. Both skip pattern making entirely, which is where the schedule and the cost usually go.
| Printed sand mould | Printed wax pattern | |
|---|---|---|
| Process | 3DP or SLS printed sand mould and core, then gravity or low-pressure casting | SLS printed wax pattern, ceramic shell, then investment casting |
| Best for | Larger parts, thicker sections, structural and housing geometry | Thin walls, fine detail, complex internal passages, tight finish |
| Outillage | Aucun | Aucun |
| Typical tolerance | CT8 to CT12 depending on process route | DCTG 4 to 6 with a silica-sol shell |
| Finition de surface | Ra 6.3 to 12.5 as cast | Ra 3.2 to 6.3 as cast |
A third route exists when the quantity justifies it: a machined steel pattern and shell cores, which is cheaper per part above roughly a few hundred pieces. If your programme is heading there, we will say so rather than quoting printed moulds indefinitely.
What tolerance will you actually get
Casting drawings are usually specified to a dimensional tolerance grade from GB/T 6414, which is the Chinese adoption of ISO 8062-3. The grade sets how much a dimension may vary with size. Lower numbers are tighter. Here is where each route normally lands.
Across our foundries the standard working figure is CT8 to CT9 with surface roughness of Ra 3.2 to 12.5. Where a part needs better than that, the fix is usually the process route rather than more machining allowance. On one aluminium pump body we held CT7 at Ra 12.3 by printing the outer mould with 3DP and the internal passage cores with SLS, because the two methods give different strengths where each one matters.
| Route | Dimensional tolerance grade |
|---|---|
| Investment casting, silica-sol shell | DCTG 4 to 6 |
| Investment casting, water-glass shell | DCTG 7 to 9 |
| Shell and machine-moulded sand | DCTG 8 to 12 |
| Hand-rammed sand | DCTG 11 to 13 |
Confirm the grade before you commit
Tolerance depends on wall thickness, section transitions and how the part is gated, not only on the process. Send the drawing and the critical dimensions, and we will tell you which grade is realistic and where to leave machining allowance. We do not promise a grade on a part we have not reviewed.
Size, weight and what we can pour
A single cast runs up to one tonne and up to 1.5 m in its largest dimension on the cast steel line. Across the group we pour roughly 3,000 tonnes of cast steel and 4,000 tonnes of cast iron a year, so a part that starts as a one-off prototype can move to serial production on the same process without a second qualification.
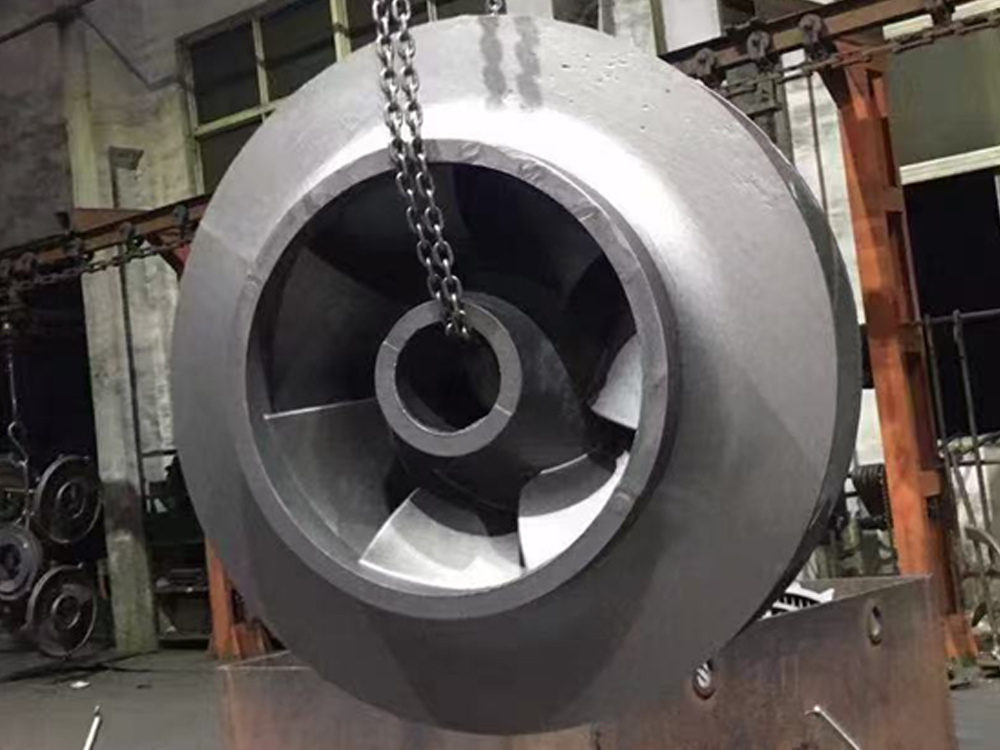
Large thin-walled pump bodyPrinted quartz-sand shell, printed ceramsite core 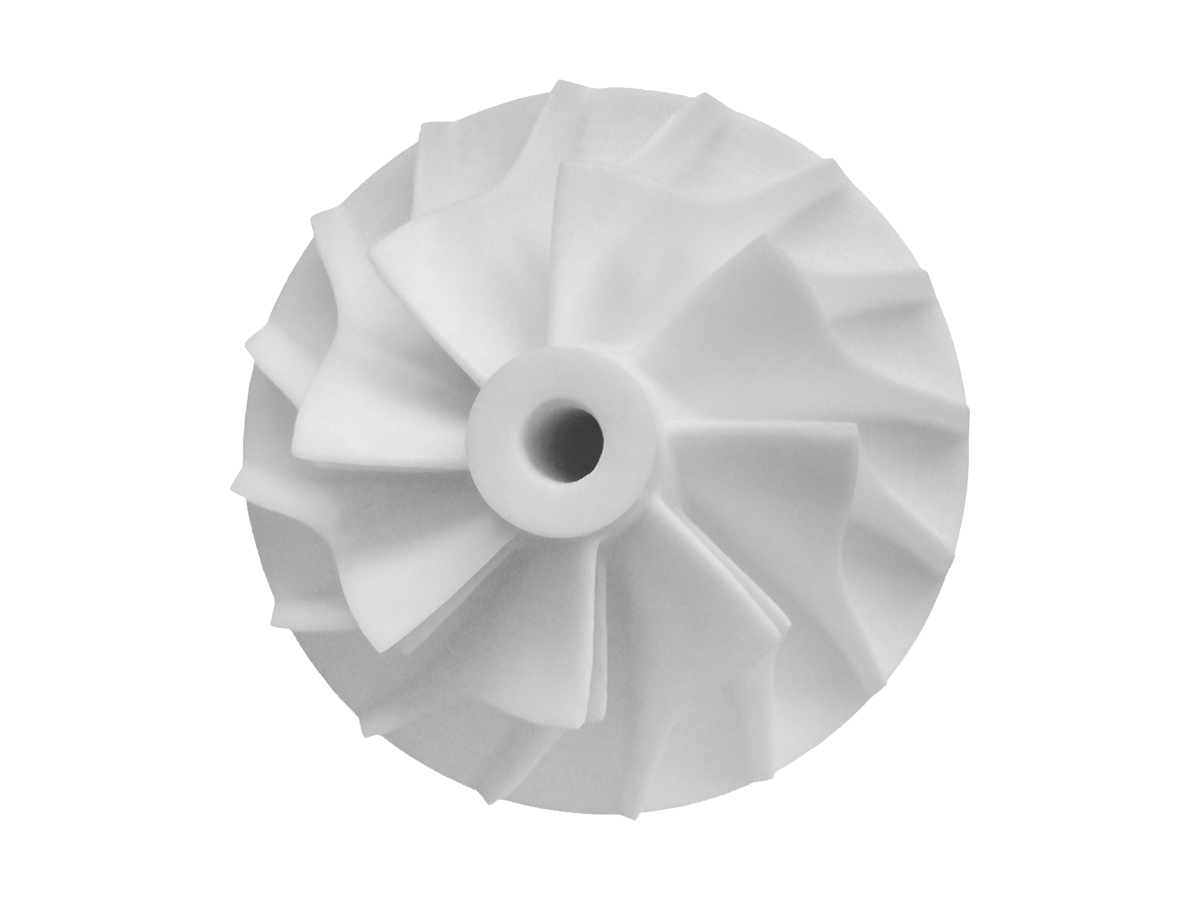
Turbine impellerHigh-temperature superalloy
A printed quartz-sand shell with a printed ceramsite core held the wall thickness and finish where a conventional pattern would have needed extra stock. The same printed-mould workflow covers nickel and cobalt alloys, not only stainless.
Two limits are worth stating plainly. Above one tonne or 1.5 m we will tell you rather than quote it, because the cast steel line is not sized for it. And a part with a section so heavy that it cannot be fed from a printed mould is better served by a forged or rolled blank — we will say so instead of quoting a casting that will pull a void.
From enquiry to delivered part
Four steps, and you know the price and the realistic tolerance before any metal is poured.
- 01
Send the model
3D model or drawing, with the alloy, the quantity and the deadline. NDA available before anything is shared.
- 02
Route and DFM review
Within 24 hours we tell you which route fits, where to leave machining allowance, and what tolerance is realistic.
- 03
Print, pour, verify
Mould or pattern printed, composition checked by spectrograph before the pour, casting poured and heat treated.
- 04
Machine, inspect, ship
CNC machining, dimensional inspection and NDT in house, then shipping worldwide from Beijing with the records.
What we run, and what comes out
Stainless is one alloy family inside a cast steel line, so the same tooling-free workflow covers duplex, nickel and cobalt superalloys where the part calls for it. Mould, core and finishing all sit in one chain, which is why a first article arrives machined rather than raw.
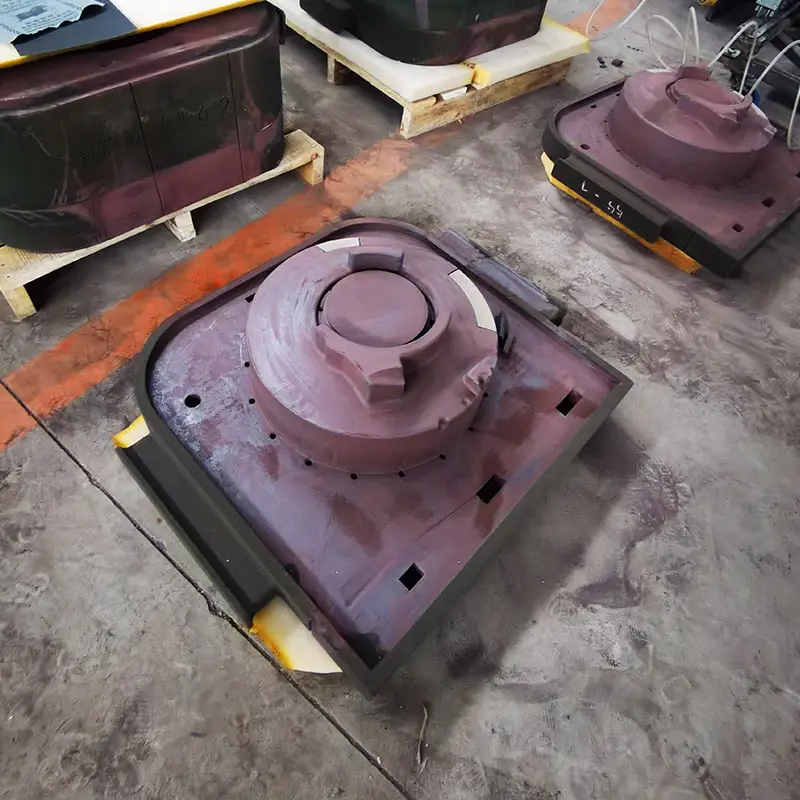
Mould ready for pouringMould and cores printed as one assembly 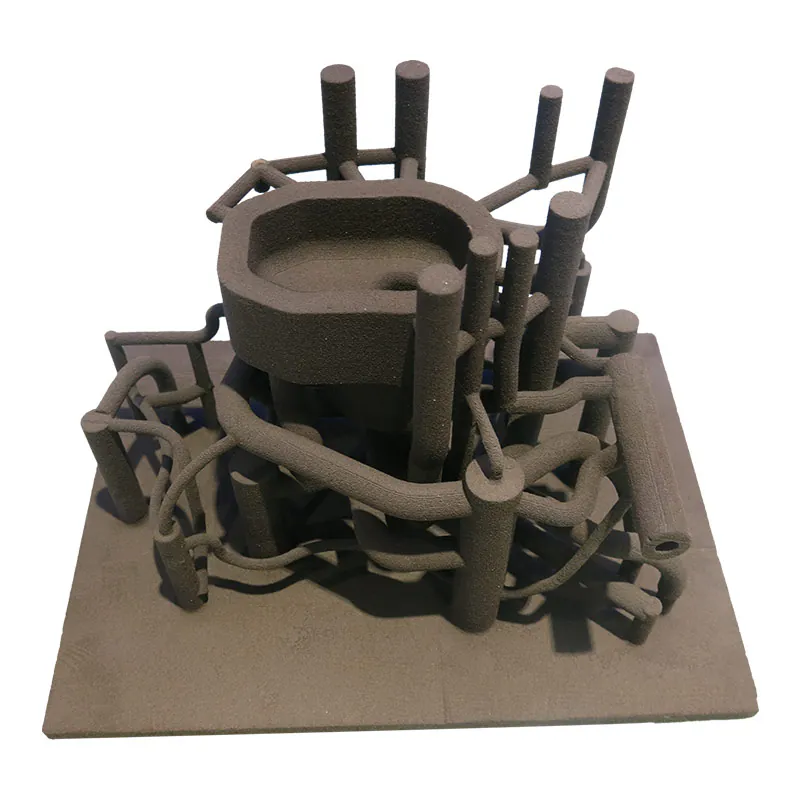
Core for a pump valve bodyInternal passage with no joint line 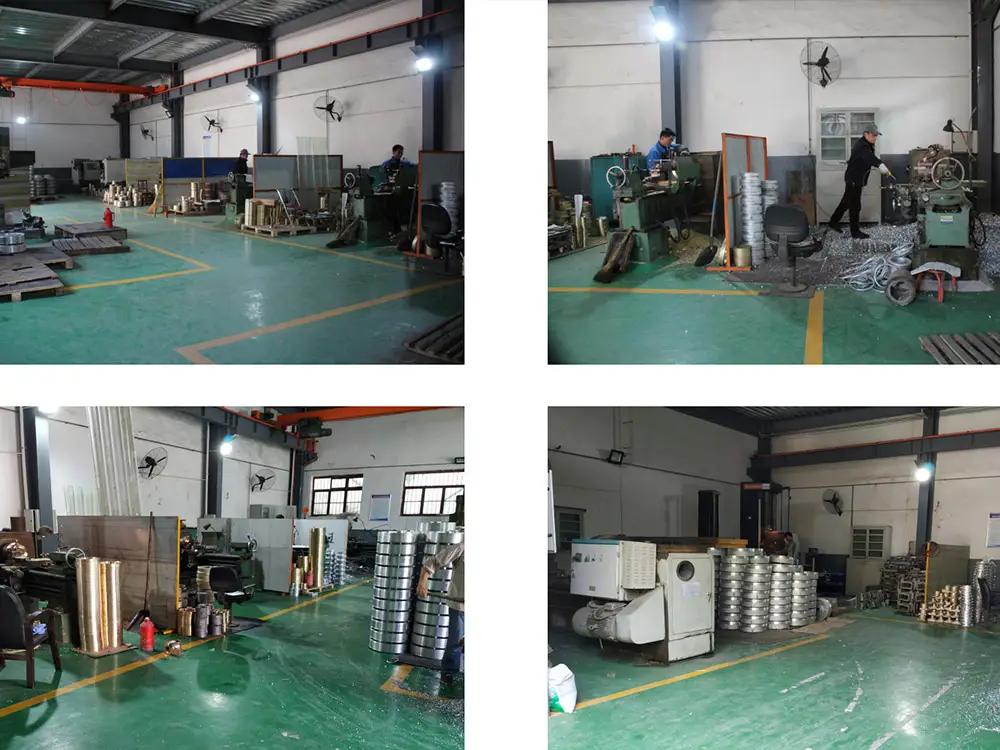
Machining and inspectionSame chain as the casting
How we keep the alloy honest
Stainless failures are usually composition failures, not shape failures. A heat that drifts on chromium or molybdenum will pass a visual check and then pit in service, so composition is verified before the pour rather than after.
- Spectrographic analysis on every heat — alloy composition is checked before pouring, not sampled afterwards.
- Nine inspection methods in house — dimensional inspection on a coordinate measuring machine and laser scanner, plus non-destructive testing before the part ships.
- Full chain under one roof — casting, heat treatment, CNC machining, surface treatment and inspection run in the same workflow, so responsibility for a rejected part is never split between suppliers.
- Traceability per heat — castings are marked so composition and process records can be traced back to the pour.
Where stainless castings from printed moulds pay off
The economics change depending on why you needed stainless and how many parts you need. Three cases come up repeatedly.
Pumps, valves and marine hardware
316 and duplex for impellers, volutes, bodies and stems exposed to chlorides. We cast a duplex pump impeller at 150 mm diameter with a 4.5 mm outlet on printed wax patterns, delivering the first small batch in 20 days at roughly half the cost of the traditional route.
Chemical and process equipment
Parts where a pinhole becomes a leak and a leak becomes a shutdown. Printed moulds allow the internal passage cores to be made in one piece, which removes the joint lines that traditional coring leaves behind.
Replacement and obsolete parts
A discontinued stainless casting with no drawing left is a common problem. Where a sample exists, it can be scanned, rebuilt as a model and cast without a pattern, which is often the only route that does not require buying tooling for a single part.
For the wider picture of what the printed-mould route covers beyond stainless, see moulage rapide. Other material routes: ductile iron casting, cast steel casting et bronze and brass casting. Related: marine, pumps and valves castings, power and energy castings, rapid prototype casting, et printing versus investment casting compared.
Questions we get before a first stainless order
Do I need to pay for a pattern or tooling?
No. Both routes print the mould or the pattern directly from your CAD file, so there is no pattern to make, no pattern to store and no pattern cost to amortise. It also means a design change between the first and second part costs nothing.
What is the smallest quantity you will run?
One part. Tooling is what normally forces a minimum order quantity in casting, and printing removes it. Most stainless work we see is prototype and validation quantities of five to fifty pieces, but single parts for fit checks are routine.
Why is stainless harder to cast than carbon steel?
It is less about temperature than about chemistry. Stainless holds a tenacious oxide film that does not float out of the melt, so a turbulent pour folds it into the casting as inclusions. It also has a narrower freezing range and lower thermal conductivity than carbon steel, which changes how the mould has to be fed and how the part cools. None of that makes it uncastable — it makes the gating and the fill rate matter more.
304 or 316 for a marine part?
316. Its molybdenum content resists pitting and crevice corrosion in chlorides, which is exactly where 304 breaks down. If the part also sees high chloride stress and temperature, duplex is worth pricing before you settle on 316.
Can you machine the casting before it ships?
Yes. CNC machining, heat treatment and surface treatment are part of the same in-house chain, so you can receive a finished part rather than a raw casting. About the only thing to decide early is where you want machining allowance left.
How do I get a price?
Send the 3D model or drawing with the alloy, quantity and deadline. We review within 24 hours. Pricing depends on alloy, wall thickness, section complexity and inspection requirements, so we quote the actual part rather than publishing a rate per kilogram that will not hold.
Send the drawing, get a straight answer
Upload your CAD file with alloy, quantity and deadline. We will tell you which route fits, what tolerance is realistic and what it costs. If printed moulds are not the cheaper route for your quantity, we will say so.