
Integrating a Sand 3D Printer into Your Foundry: A Practical Blueprint

A sand 3D printer is the easiest piece of automation in a foundry to buy and the easiest to waste. Unboxed, installed, and powered on, it will print beautiful molds all day — and if the sand supply, the mold-handling route, the core assembly bench, and the pouring floor are not integrated around it, the foundry will discover that it bought a very expensive way to produce stockpiles.
This blueprint covers the integration work that makes the machine productive: where it sits in the workflow, what the facility must provide, how sand and binder are handled, who operates it, and the pitfalls that turn successful pilots into failed projects. The sequence below is the one we use when a customer buys a machine and wants it producing in the same quarter.
Where the Printer Sits in the Foundry Workflow
A 3D printer does not replace a foundry; it replaces the pattern shop and the molder’s bench. The rest of the chain — melting, pouring, shakeout, fettling, machining, and inspection — stays exactly where it is. That is the first mental shift: integration is about inserting a digital molding station into an existing foundry workflow, not about rebuilding the foundry around the printer.
The complete digital line is a five-link chain:
- Process design — the casting is engineered in software: mold split, gating, risers, and cores are designed from the CAD model.
- 3D printing — the mold segments and cores are printed in sand, cured with binder, and cleaned of loose sand.
- Mold assembly — printed segments are joined, cores set, and the mold closed exactly like a conventionally made mold.
- Casting — metal is melted and poured into the printed mold with the same parameters used for conventional molds.
- Finishing and inspection — shakeout, cleaning, machining, and quality checks complete the part.
The how sand 3D printing works guide details links two and three; this blueprint is about making all five links flow as one line. The order of work matters: design the workflow before the machine arrives, because the printer’s position, the sand storage, and the assembly bench all depend on it.
Step 1: Define the Workflow Before You Buy
The most common integration mistake is buying the printer first and planning the flow second. The workflow must be defined against your actual part mix, because it decides which machine and which auxiliary equipment you need:
- What are you printing? Cores only, complete molds, or both? Core printing integrates differently than full-mold printing: cores move to a core-setting bench, while full molds move to the pouring floor.
- What volumes and sizes? The build volume must match your largest mold segment. A foundry printing pump bodies and engine blocks needs a different machine than one printing cores for valve bodies. The sand 3D printer buyer’s guide maps part mix to machine size.
- What is the material route? Sand arrives, is mixed with binder and hardener, is fed to the printer, and used sand is recycled. Each leg needs space, equipment, and an owner.
- Where does the finished mold go? Printed molds are fragile until assembled; the route from the cleaning station to the assembly bench to the pouring floor must be short and safe.
Define these four answers in writing, with rough quantities, and the integration plan writes itself. Foundries that skip this step spend the first three months of ownership rearranging the shop around a machine that is already in the way.
Step 2: Facility Preparation
A binder jetting sand printer is a precision inkjet machine in a foundry environment, and the environment requirements are real. The machine needs a stable, conditioned space — not a cleanroom, but a controlled one:
| Requirement | Typical value | Why it matters |
|---|---|---|
| Ambient temperature | 22–28°C | Binder viscosity and printhead behavior are temperature-sensitive |
| Ambient humidity | 30–50% | Moisture affects sand flow and binder cure |
| Floor load | 2.5–5 t/m² depending on machine | Machines weigh 6–40 t with full build boxes |
| Building height | 4.5 m and up | Large machines with overhead sand delivery are tall |
| Compressed air | 0.6–0.8 MPa, clean and dry | Printhead and vacuum systems need stable supply |
| Vibration and EMI | No strong vibration or EM sources within 50 m | Print accuracy depends on a stable machine frame |
The floor-load line is the one most often underestimated. A 4-meter-class machine weighs on the order of 27 tonnes, and a full build box of sand adds tonnes more; the foundation must be engineered for it, not discovered after installation. Power is a three-phase 380 V supply sized to the machine — roughly 10–25 kW depending on model — plus air supply at defined pressure and flow. Get the facility survey done in week one, not after the machine is on the dock.


Step 3: Materials Handling and Sand Recycling
The economics of a sand printer depend on the sand loop, and the sand loop is the part of the integration that looks trivial and is not. Sand must be mixed with a 3D-printing-grade binder and hardener, delivered to the machine in the right condition, and recovered from used molds for recycling — otherwise the machine starves or the consumables budget balloons.
The production answer is an online sand-mixing system that owns the material handling problem end to end. The units we deploy (the 3DPTEK-SM600 series) are automated mixers that vacuum-load and weigh fresh and recycled sand, inject hardener with an accuracy of ±1%, mix at rates up to 600 kg/h with fresh sand alone at 100 kg/h, and feed the printer continuously. Fresh-to-recycled ratio is adjustable online — the recommended window is roughly 1:3 to 3:1 — which lets the foundry tune mold quality against recycled-sand content. The mixer itself is a three-tonne piece of equipment with its own environment and power requirements, so it must be included in the facility plan from the start.
Three material rules keep the loop healthy:
- Use 3DP-grade resin, not casting resin. The low-viscosity binder formulated for inkjet printheads cannot be substituted with conventional foundry resin; substitution is the fastest way to clog heads and ruin molds.
- Keep sand dry and flowing. Moisture and packing are the two enemies of the recoater. Bulk sand storage must be dry, and the feed path from the mixer to the printer must be vibration-assisted.
- Recover and screen. Sand shaken out of printed molds is screened and returned to the mixing loop. Recycled content is a cost lever — every percentage point of recycled sand lowers the consumables line directly.
The material systems analysis explains why binder and sand compatibility matters, and the break-even model shows what the sand loop is worth in RMB per kilogram.
Step 4: Staffing, Training, and Process Engineering
A sand printer replaces manual molding labor with a different, scarcer skill: digital process engineering. The integration succeeds or fails on this staffing decision, and it is where most projects stumble.
The minimum crew for a one-machine cell is three roles, which can overlap in a small foundry:
- Operator — runs the machine, cleans builds, handles molds, and monitors the automated sand loop.
- Process engineer — designs molds and cores in CAD, defines gating and risers, and sets print parameters. This role decides whether the printed molds are castable, and it cannot be improvised.
- Maintenance lead — owns printhead care, the air supply, and the machine’s preventive maintenance schedule.
The staffing plan should also include the vendor relationship. A serious supplier backs the machine with a support organization: a development and engineering team that can answer process questions, service staff stationed near your region for fast response, and production bases where your people can train against real work. Verify those three resources during the purchase decision — a machine is only as reliable as the people who support it, and the Western vs. Chinese comparison explains how to contract that commitment in writing.
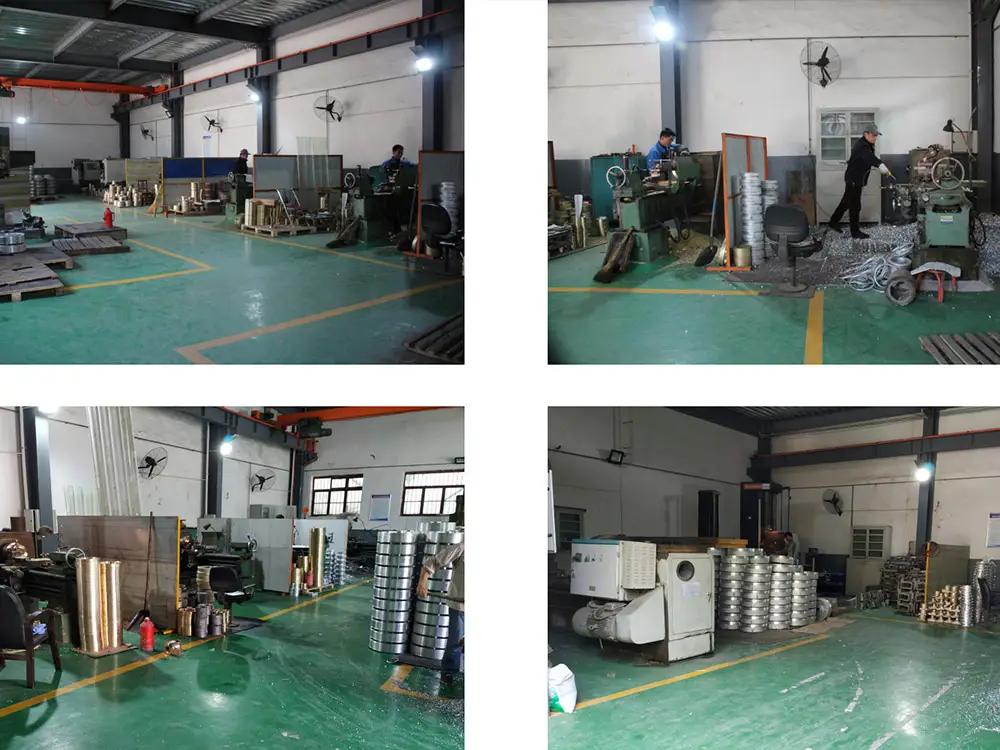
Training is a contract item, not an afterthought. A good vendor provides structured training for operators, maintenance staff, and process engineers — and, in our case, allows customer staff to train on site at the vendor’s own production bases, where the “process design + printing + casting + machining + inspection” chain is running in production. Sending two engineers for a hands-on week is worth more than a year of manuals. The training mold makers guide goes deeper into the skills ramp for exactly this transition.

Step 5: Integration with Casting and Finishing
The printed mold has to behave like a production mold on the pouring floor, and it will — with three integration details handled:
- Assembly discipline. Printed mold segments fit tightly, but they still need proper jointing, weighting, and core setting, exactly like conventionally assembled molds. The assembly bench must be sized and positioned so that a finished mold reaches the pouring floor without long carries.
- Pouring parameters. The printed mold’s sand is a furan-bonded silica or ceramic system with tensile strength in the 1.5–2.5 MPa range and gas evolution of 8–15 ml/g at 850°C. Those are conventional numbers: the same pouring, venting, and sand-control practices apply as for resin-bonded molds made by hand.
- Shakeout and recycling. The mold must be returned to the sand loop after shakeout. If the foundry’s shakeout and screening equipment cannot handle printed molds, the sand loop breaks, and the machine’s economics degrade to those of a job shop.
The rest of the line — melting, fettling, machining, inspection — needs no change, but inspection deserves one upgrade. Because the printed mold starts from a digital file, the foundry gains a quality lever it never had with hand-built tooling: the mold geometry can be verified against the CAD model. Production facilities in the integrated chain typically carry coordinate measuring machines, laser 3D scanners, and vacuum direct-reading spectrometers, so mold dimensions, casting geometry, and alloy chemistry are checked against the file and the specification at every stage. That closed loop is what lets a digital molding line hold repeatability that manual molding cannot — and it is a strong argument for routing pilot programs through the printed line from the start. A foundry with an existing resin-sand line has 80% of the integration already done; the printer replaces the pattern and the molding bench, not the foundry. The one-stop workflow explains the full chain from file to finished casting.
Automation: Running Unattended
The final integration layer is automation, and it is what turns the machine from a cost center into a production asset. Modern sand printers run unattended through nights and weekends with the right support systems:
- Overhead sand delivery. Bulk bags (ton bags) are staged above the feed system, and sand is mixed and conveyed to the printer automatically.
- Online mixing and monitoring. The mixer runs the sand loop unattended, with live status monitoring and automatic alarm on faults.
- Remote monitoring. Print jobs, material levels, and machine status are visible remotely, so one person supervises several machines and can react before a failure stops the build.
Supervision follows a simple pattern: one person owns the cell, checks the monitor before and after each pour shift, and lets the machine work through the hours when the foundry is quiet. Faults trigger alarms that reach the supervisor remotely, so a stopped build costs minutes instead of a shift. The practical effect is utilization: a machine that runs 24 hours with a night-shift skeleton or no night shift at all produces the 7,000+ hours per year that the payback benchmarks assume. Automation is not a luxury on top of integration; it is the difference between a printer that funds itself and a printer that needs funding.
Pitfalls to Avoid
The failures we see in customer integrations are consistent enough to list. Avoid these seven and the project is most of the way home:
- Buying before planning the flow. The machine arrives and the shop rearranges around it, costing months.
- Under-budgeting facility work. Floor load, height, power, air, and HVAC are real capital; skipping them means a machine that cannot run at spec.
- Using the wrong binder. Substituting conventional casting resin to save money clogs printheads and voids the process guarantee.
- No process engineer. Operators can run the machine, but only a process engineer can design a castable mold. Without one, the machine prints scrap.
- Skipping the sand loop. No mixer and no recycling means manual feeding and full-cost consumables — the economics of article 22 never materialize.
- Treating the printer as a separate island. If molds cannot reach the pouring floor efficiently, the printer’s speed is wasted.
- Ignoring maintenance. Printheads are wear items with a defined service life; a maintenance schedule and spare heads are part of the operating plan, not an emergency budget.
Each pitfall maps to a step in this blueprint, which is the point of writing the integration down before the equipment order.
The 90-Day Integration Timeline
A realistic integration from purchase order to first production castings fits in about one quarter. The table below is a template:
| Phase | Weeks | Deliverables |
|---|---|---|
| Workflow & facility plan | 1–3 | Part mix analysis, machine selection, layout, facility survey |
| Facility work | 3–8 | Foundation, power, air, HVAC, sand storage, mixer installation |
| Machine install & commissioning | 6–9 | Unpacking, installation, calibration, acceptance tests |
| Training | 8–12 | Operator, process engineer, maintenance training; trial molds |
| First production castings | 10–13 | Pilot parts poured, inspected, and delivered; sand loop tuned |
The critical path is almost always the facility work, not the machine. Starting the facility survey in week one is what makes the 90-day timeline realistic; starting it after delivery adds a quarter. A vendor with production bases of its own can compress the training and pilot phases, because your engineers can practice on equipment that is already running — the service provider selection guide explains what to look for in an integration partner.
Once the first pilot castings pass inspection, the integration work shifts from building the line to tuning it: adjusting gating and risers on printed molds, optimizing recycled-sand ratios, and expanding the part list that routes through the printed line. The 90-day timeline ends with the machine no longer being a project — it is simply how the foundry makes molds, and the next printer purchase follows the same blueprint.
Frequently Asked Questions
How long does it take to integrate a sand 3D printer? A realistic integration from purchase order to first production castings is about one quarter: workflow planning and facility work in the first two months, installation and training in the third, and pilot castings by week 12–13. Facility work is usually the critical path.
What facility requirements does a sand 3D printer have? A controlled environment at 22–28°C and 30–50% humidity, a floor rated for the machine (2.5–5 t/m² depending on model), 4.5 m of building height, three-phase power at 10–25 kW, and clean dry compressed air at 0.6–0.8 MPa.
Do I need a special sand-mixing system? For production use, yes. An online mixer (such as the 3DPTEK-SM600) weighs, mixes fresh and recycled sand with hardener at ±1% injection accuracy, and feeds the printer continuously. Manual feeding is possible for pilots but does not scale.
Can a sand 3D printer run unattended? Yes, with the right support systems: overhead ton-bag sand delivery, an automated mixing loop, online monitoring, and remote access. Unattended operation is what enables the 7,000+ hours per year that make the machine’s payback work.
What staff do I need to run it? Three roles: an operator, a process engineer who designs molds and cores in CAD, and a maintenance lead who owns printhead care. The process engineer is the role most foundries lack and the one that decides whether printed molds are castable.
Can I use my existing casting resin in the printer? No. 3D printing uses a low-viscosity furan binder formulated for inkjet printheads; conventional casting resin will clog the heads and degrade mold quality. The binder is a standard consumable, not an expensive mystery.
Does the printer replace my existing molding line? It replaces the pattern and the manual molding bench for the parts routed through it. Melting, pouring, shakeout, fettling, machining, and inspection remain unchanged, so a foundry with an existing resin-sand line has most of the integration done already.
How do I plan the integration for my foundry? Start with the workflow definition — what you print, at what size and volume, and how molds reach the pouring floor — then survey the facility before ordering. Request an integration plan with your part mix and layout and the team will return the workflow, equipment list, and facility checklist.


