
Стоимость металлического 3D-принтера в 2026 году: сколько на самом деле платят литейные предприятия

The sticker price of a metal 3D printer is the smallest number in the decision. A foundry that budgets only for the machine discovers the truth in the second year, when powder, argon, sintering furnaces, and maintenance have quietly spent the machine’s value again. Metal printing is a capital purchase, but the purchase that matters is the cost per good part, and that depends on technology choice, utilization, and the post-processing line behind the printer.
This article breaks down what metal 3D printers actually cost in 2026 — machines from entry research units to industrial production systems, the consumables that keep them running, the post-processing that nobody quotes up front, and a total cost of ownership framework for foundry buyers. The prices below are realistic market ranges, because configuration, options, and location move every quotation.
The Real Cost of a Metal 3D Printer: More Than the Machine
A metal additive manufacturing cell is four cost layers stacked on top of each other:
- The printer. The machine that builds the part, from small research systems to large-format industrial units.
- The consumables. Metal powder, binder (for binder jetting), argon or nitrogen gas, filters, and recoater blades.
- The post-processing line. Debinding and sintering furnaces for binder jetting, heat treatment and support removal for powder bed fusion.
- The operation. Operators, engineers, facility conditioning, maintenance, and scrap rework.
Foundry buyers usually compare only the first layer. The second and third layers are where the technologies diverge, and the fourth layer decides whether the investment pays back. That is why the two mainstream metal technologies — selective laser melting and metal binder jetting — can have similar machine prices and completely different cost-per-part economics.
Entry, Mid-Range, and Industrial Machines
Metal printers cluster into three tiers, and the tier determines the build size, throughput, and price. The table below shows the typical 2026 market range for each tier. Treat the figures as indicative; the final number is configuration-dependent and subject to the vendor’s quotation.
| Tier | Typical build envelope | Ориентировочный диапазон цен | Who buys it |
|---|---|---|---|
| Research / entry | 100–300 mm in the largest axis | $150k–$400k | Universities, R&D labs, first adopters |
| Production mid-range | 250–400 mm, single or multi-laser | $400k–$900k | Job shops, medical and tooling producers |
| Industrial large-format | 500 mm and up, multi-laser or large BJ build boxes | $1M+ | Aerospace, automotive, high-volume production |
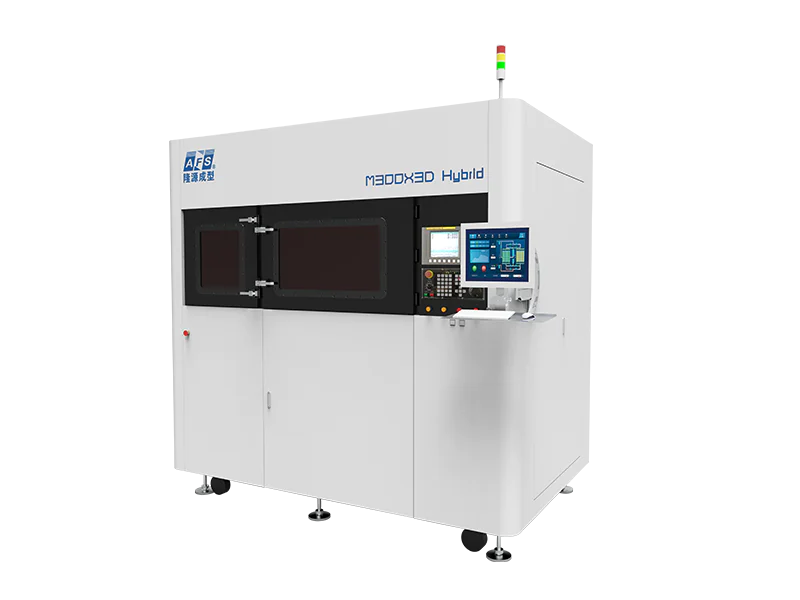
The same tiers exist in both technologies. In the powder bed fusion family, AFS-M120X и AFS-M120TX systems are research- and gradient-material platforms, the AFS-M300XAS covers the production mid-range, and the AFS-M400 is a 3C-electronics dedicated production machine. In the binder jetting family, the 3DPTEK-J160R is a research platform with a 160 × 65 × 65 mm build, while the 3DPTEK-J400P and 3DPTEK-J800P move into production, with the J800P offering an 800 × 500 × 400 mm build at 8 L/h of metal volume.
Technology Choice 1: Powder Bed Fusion (SLM/LPBF)
Powder bed fusion melts metal powder with a laser, layer by layer, into a fully dense part. The process is the industry standard for high-value parts in titanium, tool steel, stainless, and nickel alloys, and it is the technology most foundry buyers picture when they hear “metal 3D printing.”
The cost structure is honest about its weaknesses:
- Machine capex is the headline: single-laser entry systems at the low end of the range, multi-laser industrial systems at the top.
- Argon consumption is continuous. The build chamber must be purged and maintained under inert gas, and argon is a recurring line item that scales with build time.
- Support structures are mandatory for overhangs. They add material, build time, and a manual removal step, and they leave witness marks that often need machining.
- Throughput is serial. One laser, one layer, one part at a time. Build rates are far below what batch production needs, which is why cost per part stays high at volume.
Where SLM shines is material performance and geometry freedom for critical parts. A titanium component with internal cooling channels, or a tool-steel insert with conformal cooling, justifies the technology because no other process makes the part at all. The metal binder jetting vs. SLM comparison goes deeper into the technical trade-offs; for cost, the rule of thumb is that SLM wins on performance-critical one-offs and small series, and loses on volume.
Technology Choice 2: Metal Binder Jetting
Metal binder jetting builds parts the way sand 3D printing builds molds: a printhead selectively deposits binder onto a bed of metal powder, layer by layer. The “green” part is then debound and sintered into dense metal in a furnace, using the same downstream process as metal injection molding.
The economics are structurally different from laser melting:
- No lasers, no argon. The build step is an inkjet process, so the inert-gas and laser costs disappear from the per-part equation.
- Batch throughput. The printhead deposits binder across the whole bed, so the cost per part collapses as the build box fills. Our internal benchmark against laser melting is roughly 50× faster build speed and about one-fifth of the cost at comparable volumes — figures the binder jetting guide explains in process terms.
- Powder reuse is favorable. Binder jetting uses fine powders in the 5–25 μm range, the same specification as metal injection molding feedstock, which keeps powder cost below typical SLM grades.
- Shrinkage is controlled, not free. Sintering shrinks the part predictably — around 15–16% for stainless steel and 14–15% for titanium — and that shrinkage must be compensated in the digital model. It is an engineering cost, not a per-part cost.
The process handles a wide material map: 304 and 316L stainless, mold steel, titanium alloys (sintered tensile strength above 1,000 MPa in production parts), copper alloys, tungsten, aluminum, high-temperature alloys, and silicon carbide ceramics. Parts come out at 98%+ sintered density from green densities above 60%.

Binder Jetting vs SLM: Price per Part
The machine price is only half the story; the cost per good part is the number that funds the machine. The table compares the two technologies across the cost drivers that matter to a foundry:
Machine-level figures first: the binder jetting 3D printer price bands show what each machine class costs before you get to the per-part math below.
| Cost driver | SLM / LPBF | Metal binder jetting |
|---|---|---|
| Machine cost (comparable tier) | Similar to high, laser and scanner content | Similar to lower, printhead content |
| Gas consumption | Continuous argon | Нет |
| Build speed | Serial, laser-limited | Batch, bed-wide deposition |
| Powder specification | Coarser, costlier grades | Fine 5–25 μm, MIM-compatible grades |
| Support structures | Required, add material and labor | Not needed; loose powder supports |
| Post-processing | Heat treat, support removal, machining | Debind + sinter furnace, then machining |
| Best cost position | 1–10 parts, high-value alloys | 50–10,000 parts, batch production |
The crossover point depends on part size and quantity, but the direction is consistent: laser melting is the right tool for critical geometry in small numbers, and binder jetting is the right tool when volume appears. That is why the industry has positioned binder jetting as the batch-production technology — the same logic that made the open vs. closed material systems debate central to buyer decisions.
Consumables: Powder, Binder, and Filters
Consumables are the recurring cost that separates a good quotation from a profitable one. In powder bed fusion, the big items are metal powder, argon, and recoater consumables. Powder is bought in kilograms, sieved and reused across builds, but the recycle rate is never 100%, and powder degrades in quality with each pass. In binder jetting, the recurring costs are powder plus the binder itself, which is dispensed through the printhead at high resolution.
Binder formulation is a hidden differentiator. A proprietary binder that must be bought from the machine vendor creates a captive consumables stream; a binder that works with standard powders and an open material list keeps the foundry in control of its costs. Our binder jetting systems run a self-developed binder family with more than 20 formulations across five series, which matters for two reasons: it is tailored to the metal being printed, and it keeps consumable pricing predictable. The material-system economics are covered in the open vs. closed material systems analysis, including how binder cost scales with part volume.
Metal powder is not a place to save money. Powder quality controls final density, mechanical properties, and consistency between batches, so buyers should budget for certified powder from the start and verify the supplier’s specification against the machine’s material map.
The Post-Processing Line Nobody Quotes Up Front
The largest hidden cost in metal printing is the finishing line. For binder jetting, the green part must be debound and sintered, which means a debinding furnace and a high-temperature sintering furnace, with controlled atmosphere. This is real capital: sintering furnaces are substantial investments, and they add floor space, gas supply, and qualification work. The good news is that the sintering step is the same process metal injection molding has used for decades, so the equipment, materials, and standards are mature — a foundry moving from MIM or powder metallurgy already owns this line.
For powder bed fusion, the post-processing is different but no cheaper: heat treatment, support removal, and often CNC finishing on functional surfaces. Support removal is manual labor, and it is easy to underestimate. A dense batch of small parts can spend more operator hours on support removal than on the build itself.
The practical rule: add the post-processing line to the budget before the printer. A metal printing cell without a finishing line is a printer that cannot ship parts. Buyers who plan the furnace, the atmosphere supply, and the labor together get real utilization; buyers who buy the printer first wait months while the finishing line is installed.

Buy vs. Outsource: When the Machine Isn’t the Answer
Before any foundry signs for a metal printer, it should answer one uncomfortable question: will this machine run enough hours to pay for itself, or would the same parts be cheaper bought as a service? The threshold is utilization, and it is brutally honest. A machine that builds for eight hours a day, five days a week, pays back on a normal five-year schedule. A machine that builds two days a week is a museum piece with a maintenance budget.
Outsourcing changes the numbers. A service bureau prices parts at a margin that includes machine depreciation, so it looks expensive per part — until the foundry counts the cost of running its own cell at 15% utilization. For one-off prototype batches, pre-production runs, and occasional replacement parts, a qualified metal printing service is often the cheaper answer, with zero capex and instant access to the latest material and build options.
The decision rule is a volume threshold. Estimate your stable monthly metal part volume across the next three years. If that volume fills less than roughly a third of a production machine’s capacity, keep buying parts as a service and revisit the decision when volume grows. If the volume is there — or if lead time and IP control are strategic — the machine earns its place, and the same logic that drives buying versus renting a sand 3D printer applies to metal.
There is a middle path that is underused: start with a research-class system such as the 3DPTEK-J160R or the AFS-M120X, qualify the process and the materials on real parts, and step up to a production system only when the utilization forecast justifies it. This staged approach limits the downside of a wrong-size purchase and turns the first machine into the training platform for the second.
Hidden Costs: Facility, Gas, Maintenance, and Training
Four operating costs are routinely under-budgeted by first-time buyers:
- Facility conditioning. Metal printers are sensitive to ambient temperature and humidity, and they need clean, vibration-free floors with defined load capacity. A 120 mm-class SLM system already requires about a tonne per square meter of floor load; production binder jetting systems such as the J800P need 3 t/m². Concrete, HVAC, and electrical upgrades can cost as much as a small machine.
- Gas supply. SLM systems need a clean, dry compressed-air and argon supply at defined pressure and flow. The supply line must be sized before installation, not after.
- Maintenance. Printheads, recoater blades, filters, and laser optics are wear items. Budgeting 2–4% of machine value per year for consumable maintenance is a realistic planning number, and uptime depends on the vendor’s service coverage.
- Training. An operator who understands process parameters, powder handling, and sintering profiles is worth more than the machine. Budget for structured training and one engineering hire per cell, not “we will learn as we go.”
These costs are also why the Western vs. Chinese 3D printer comparison matters more than the sticker price: support coverage, spare-part lead times, and service responsiveness are TCO items, not marketing claims. TCO beats sticker price as a comparison method. The 3D sand printer ROI article applies the same discipline to sand printing, and the sand 3D printer break-even model shows the spreadsheet logic in detail — the same framework transfers to metal.
Total Cost of Ownership: A Foundry Buyer’s Checklist
Before requesting quotations, a foundry buyer should assemble a five-year TCO model. The checklist below is the minimum:
- Machine price — base unit, options, installation, commissioning.
- Facility work — floor load, height, HVAC, electrical, gas lines.
- Consumables — powder per kg and per part, binder or gas per build, filters.
- Post-processing — furnace capex and operation, or outsourced sintering cost.
- Труд — operators, engineers, and training across five years.
- Maintenance and downtime — service contracts, spare parts, and lost-utilization cost.
- Utilization forecast — honest part volume per month, not the brochure’s maximum speed.
For foundries already casting titanium and other reactive alloys, the comparison extends to whether the printed part replaces a casting, a forging, or a machined billet — each has a different baseline cost, and the metal printing cell must beat its own baseline, not just a competitor’s machine. The last line is the one that funds the decision. A $600k machine at 20% utilization loses to a $400k machine at 60% utilization. Binder jetting’s batch economics reward filling the build box; SLM’s serial economics reward high-value geometry. Match the technology to the utilization forecast, and the TCO model does the rest. The cost of 3D sand printing analysis shows the same methodology applied to mold and core production, which is useful context because many foundries buy a sand printer first and a metal cell later.
Applied to the 3DPTEK range: entry and mid-range binder jetting starts with the 3DPTEK J160R и 3DPTEK J400P, production volume with the 3DPTEK J800P, and the SLM comparison point is the AFS-M120.
If the arithmetic above is the reason you are buying parts instead of a machine, we print them. Materials, tolerances and inspection are on the metal 3D printing service page.
Часто задаваемые вопросы
How much does a metal 3D printer cost in 2026?
Research-class systems start around $150k, production mid-range systems run from roughly $400k to $900k, and large-format industrial systems exceed $1M. Configurations, options, and region move every quotation; treat these as planning ranges, not prices.
What is the difference between SLM and binder jetting cost?
SLM spends on lasers, argon, and serial build time; binder jetting spends on powder, binder, and a sintering furnace. At comparable utilization, binder jetting reaches roughly one-fifth of the per-part cost as volumes grow, with a far faster build step.
Why does binder jetting need a sintering furnace?
Binder jetting produces a green part of powder held by binder; sintering densifies it to 98%+ density in a furnace. The debind-and-sinter step is the same mature process used by the metal injection molding industry.
Do metal 3D printed parts shrink?
Yes. Binder-jetted stainless steel shrinks about 15–16% during sintering, and titanium about 14–15%. Shrinkage is compensated in the digital model and controlled by the print and sinter parameters.
Which is cheaper for production: SLM or binder jetting?
For batch production of tens to thousands of parts, binder jetting is generally cheaper per part. For one-offs and small series in high-value alloys where geometry is critical, SLM is often the right — and cheaper — choice.
Can binder jetting print titanium and copper?
Yes. The material map includes 304/316L stainless, mold steel, titanium alloys, copper alloys, aluminum, tungsten, high-temperature alloys, and ceramics such as silicon carbide. Sintered titanium parts exceed 1,000 MPa tensile strength in production.
How much powder does a metal printer use?
It depends on part volume and build-box packing. Powder is reused with sieving, but recycle rates are not 100%, so budget for make-up powder per build. Binder jetting uses fine 5–25 μm powder at MIM-compatible grades, which are generally less costly than coarser SLM grades.
How do I compare quotations from different vendors?
Build a five-year TCO model covering machine, facility, consumables, post-processing, labor, and maintenance, and divide by your realistic utilization forecast. The vendor with the lowest sticker price rarely wins that comparison.
What is the total investment for a metal printing cell?
A complete cell — printer, finishing line, facility work, and first-year operation — typically runs 1.5× to 2.5× the printer price alone. Plan the full cell before signing for the printer, or request a proposal that includes the post-processing line in the quotation.
Рекомендуемые материалы
SLS 3D printer cost breakdown · 3D sand printing cost · binder jetting guide.


