
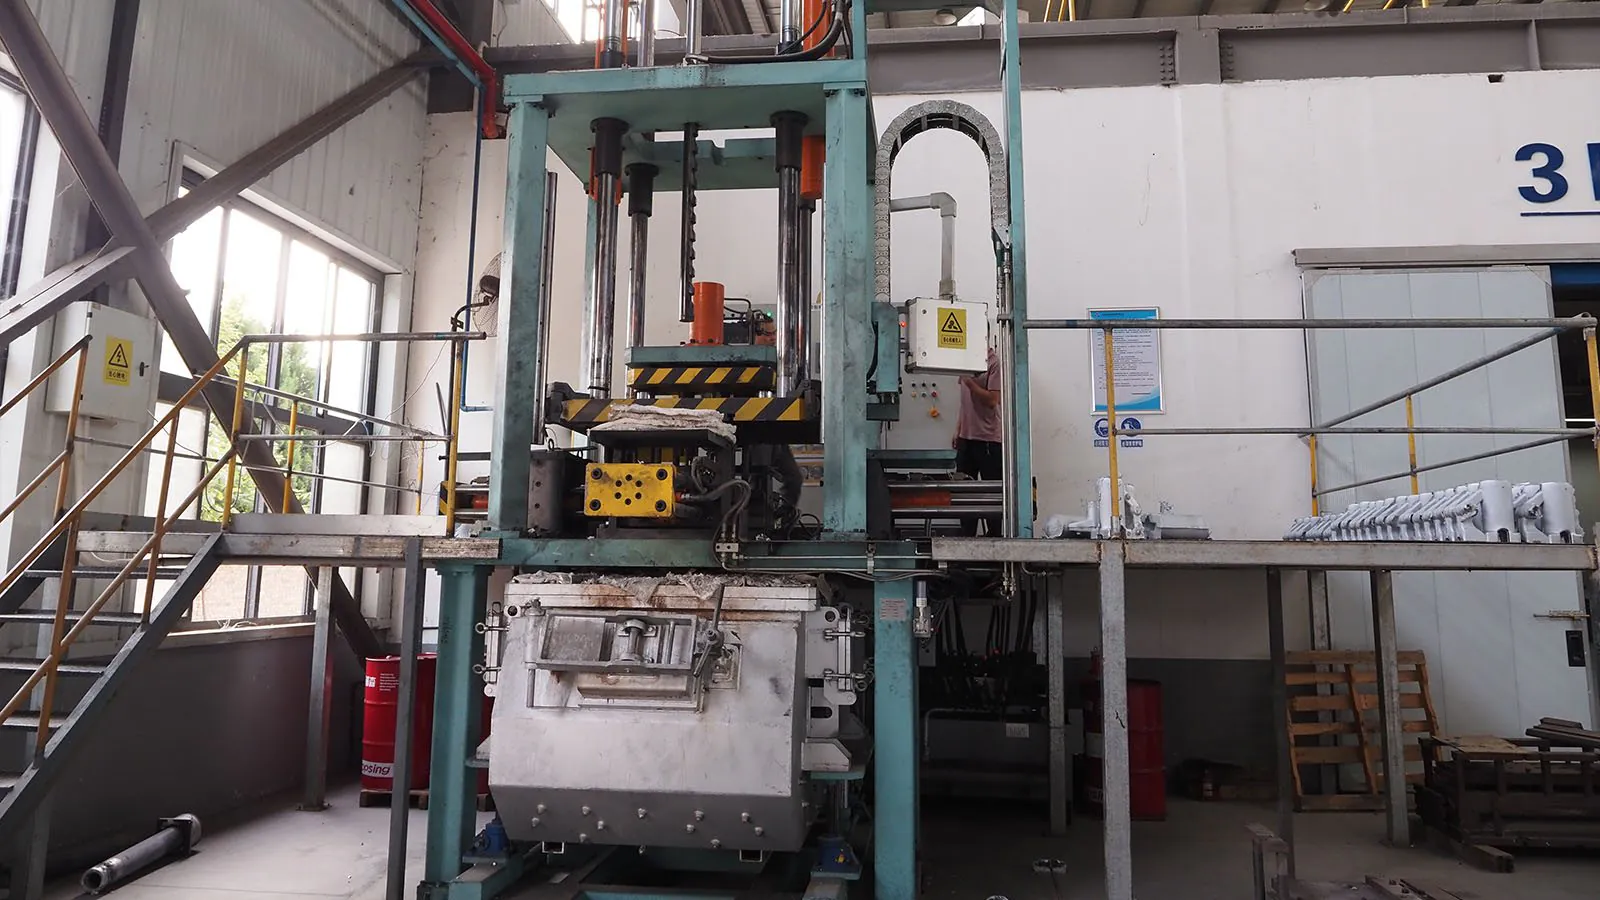
Low pressure casting for pressure-tight aluminium parts, without a die
Low pressure casting fills the mould from below, pushing metal up a riser tube with nothing more than dried compressed air. The fill is slow and laminar, the riser keeps feeding as the part freezes, and the result is a dense, pressure-tight casting with almost no feeder metal to cut off. We run it into printed sand moulds, so there is no die and no pattern — a single switchgear housing is a normal order.
What low pressure casting is, and when it is the right process
The mould sits on top of a sealed furnace. A ceramic riser tube reaches down into the melt, and dry compressed air at a fraction of a bar presses the metal up that tube and into the cavity. Because the metal rises into the mould rather than being poured into it, it fills quietly — no turbulence, no folded oxide film, no gas dragged in behind the stream.
The second advantage is what happens after the fill. The riser tube stays full of liquid metal and remains the last thing to freeze, so it feeds the casting as it contracts. Solidification runs from the far end of the cavity back towards the gate, which is the direction you want. That is why low pressure parts come out pressure-tight where a gravity pour of the same geometry can leak, and why the process needs almost no feeder metal — the yield is high and the cut-off is a single stub.
If your part is an aluminium housing with an internal cavity that has to hold gas or oil, low pressure is usually the process. If it is a simple structural part with no pressure duty, gravity casting is cheaper. If you need tens of thousands of parts a year, none of the sand processes are the answer — that is die casting, and we do not run it.
Low pressure, gravity or die casting
Three processes, three different answers to the same question: how does the metal get into the cavity, and how does it behave once it is there. The choice is usually decided by whether the part has to be pressure-tight, and by how many you need.
| Property | Low pressure | Gravity | High pressure die |
|---|---|---|---|
| How the metal enters | Pressed up a riser tube | Poured into the sprue | Injected at speed |
| Filling behaviour | Slow and laminar | Gravity, some turbulence | Fast and turbulent |
| Pressure-tightness | Best of the three | Moderate | Good, but gas porosity risk |
| Casting yield | High — one riser stub | Lower, heavier feeders | High |
| Tooling | Printed sand mould, no pattern | Printed sand mould, no pattern | Hardened steel die |
| Economic at | 1 part upwards | 1 part upwards | Tens of thousands a year |
| Wall thickness | Thin to medium | Medium | Thin |
| Cycle time | Slower | Slow | Fastest |
| Typical parts | Switchgear and GIS housings, motor housings, wheels | Brackets, covers, simple structural parts | Small precise components at volume |
Five low pressure cases, documented
Every part below is aluminium ZL101A, cast low pressure into a printed sand mould, in small batch, and delivered in 20 days from the drawing. All five reached Class 1 dimensional accuracy and were delivered fully machined. They come from high-voltage switchgear and gas-insulated switchgear duty, where a housing that leaks is not an option.
| جزء | Size | Dimensional result | Delivered |
|---|---|---|---|
| Contact base | 400 × 85 mm | Class 1 | Fully machined |
| Cylinder | 500 × 80 mm | Class 1 | Fully machined |
| Corona shield | 650 × 150 mm | Class 1 | Fully machined |
| Conductor | 2,250 × 420 mm | Class 1 | Fully machined |
| Vessel | 800 × 600 mm | Class 1 | Fully machined |
The conductor is the one worth looking at twice. At 2,250 mm it is longer than most low pressure machines are usually asked to feed, and it was made without a die — the mould was printed, poured and finished inside the same 20 days as the rest of the batch.
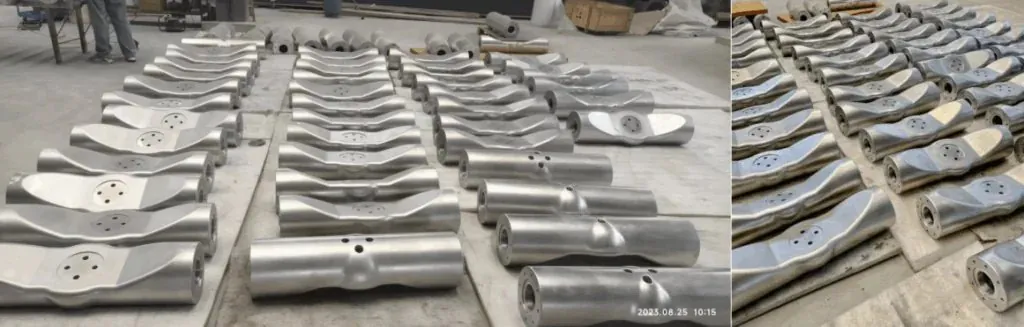
The same line runs gas-insulated switchgear enclosures for ultra-high voltage transmission. Those are the parts that made the process worth building around: internal geometry that has to be gas-tight, wall sections that vary across the part, and quantities that never justify a steel die.
The cycle, step by step
Four things happen in order, and the whole point of the process is in the second and third of them.
- 01
Seal and connect
The printed sand mould is clamped onto the furnace and a ceramic riser tube is brought up into the melt. The furnace is sealed, because the next step depends on the only opening being the tube.
- 02
Pressurise and fill
Dry compressed air at a fraction of a bar pushes metal up the tube and into the cavity. The pressure is held low and the fill rate is controlled, so the metal rises as a quiet front rather than a jet.
- 03
Hold while it freezes
Pressure is maintained after the cavity is full. The riser is still liquid metal under pressure, so it feeds the shrinkage as the casting solidifies from the far end back towards the gate.
- 04
Release and finish
Pressure is vented, the mould comes off, and the metal left in the tube is recycled. What is left on the casting is a single stub to cut, then machining and inspection.
Why the mould is printed
Conventional low pressure casting runs into a metal die, which is why it is normally a volume process. We run it into a printed sand mould instead. The mould is printed from your CAD file in a few days, so there is no die to cut, no pattern to store, and no minimum quantity — the process that used to need a die is now available at one part.
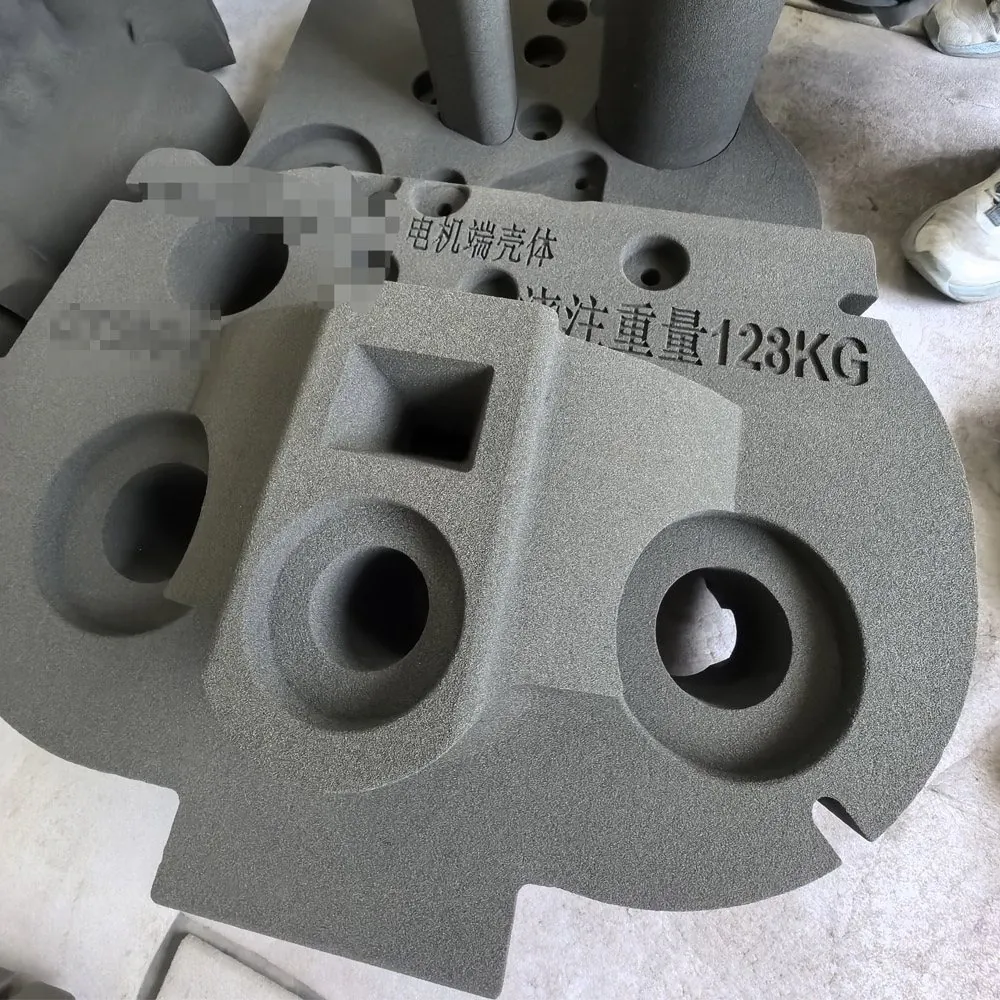
Mould for a motor end housingPrinted from CAD, cores included 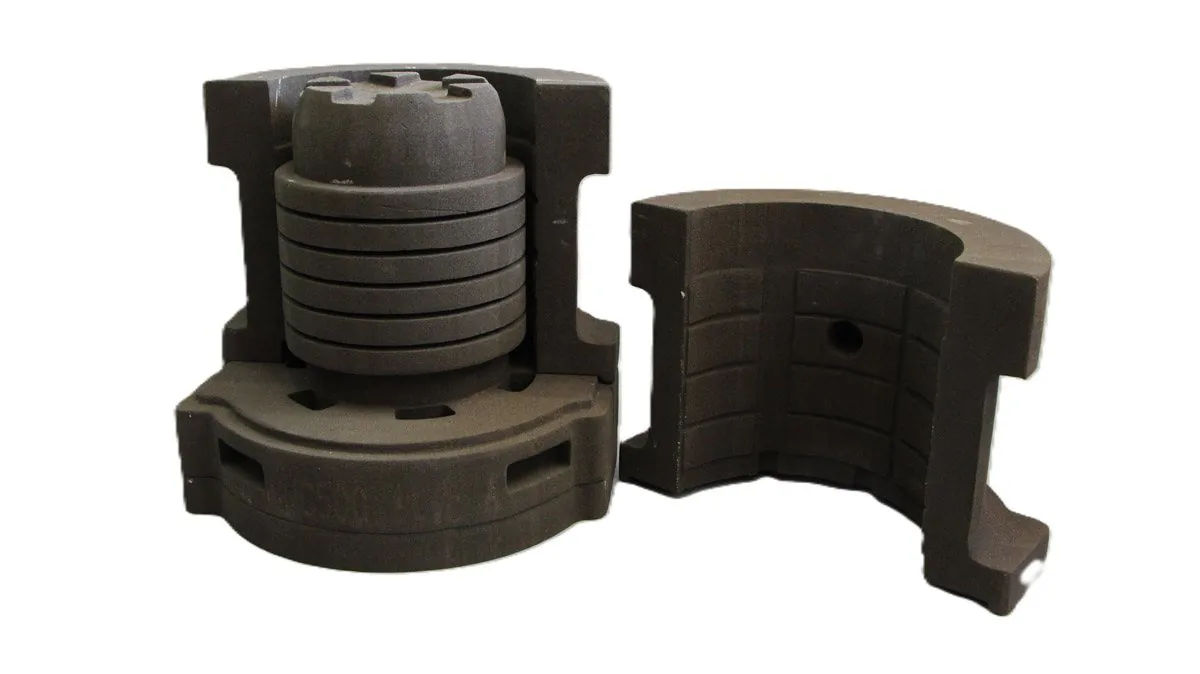
Core assembly for a water-cooled casingPrinted cores, glued as one set 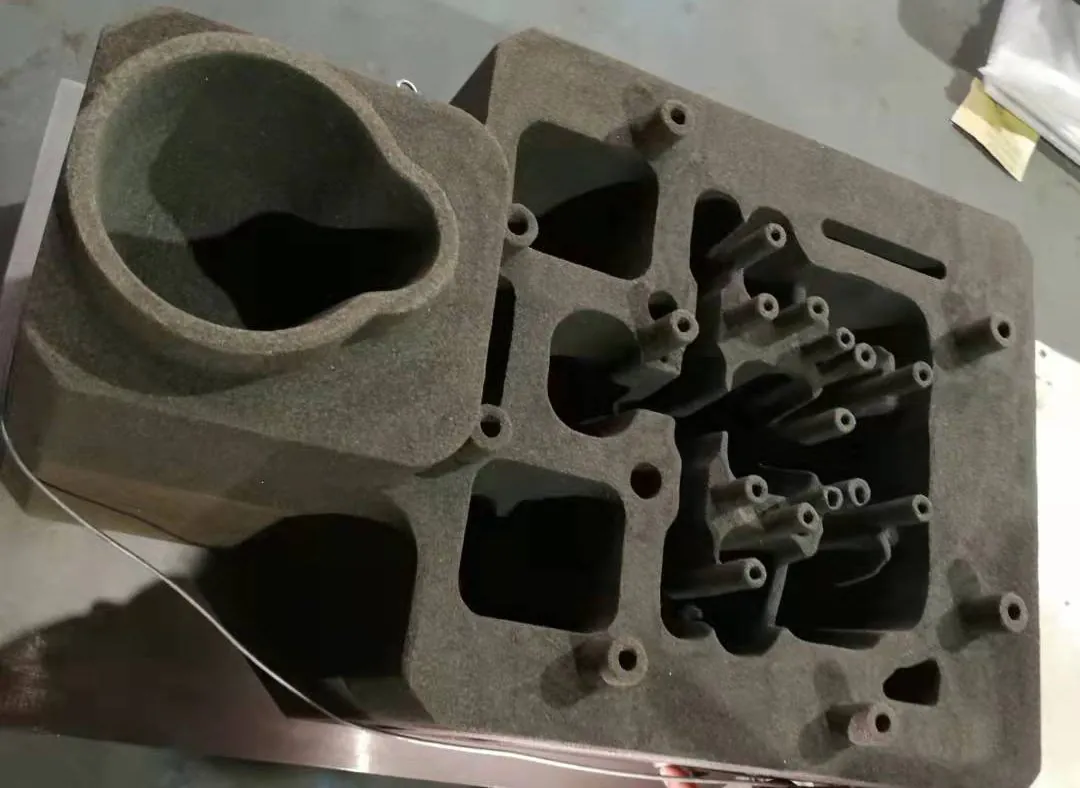
Mould and cores for a cylinder headInternal passages in one setup
The mould-making cycle runs about 70% shorter than the traditional route, and the printed surface comes out at around Ra 25µm against Ra 50µm or worse from a rammed sand mould. Printed moulds are made from silica or ceramic sand with furan resin — the same chemistry a conventional no-bake line runs, so the mould behaves the way a foundry expects.
The moulds come off our own machines: the 3DPTEK-J1800 for moulds and cores up to about a metre, the 3DPTEK-J4000 for the large work. See the full sand printer range.
What decides whether a low pressure casting passes
Low pressure removes some defects by design and introduces a couple of its own. The process either makes a dense part or it makes a part with holes in it, and which one you get comes down to these six.
Wet or oily pressurising air
The air that pushes the metal in is in direct contact with the melt surface. Moisture or oil in that air goes straight into the metal as hydrogen, and comes out as porosity in the last section to freeze. Dried, filtered air is not optional.
Fill rate matched to wall thickness
Too slow and the metal freezes before the cavity is full — a misrun or a cold shut. Too fast and it stops being laminar, which is the whole reason for using the process. The pressure ramp is set against the thinnest section, not the average.
Solidification order
The riser only feeds while it is still liquid. If a heavy section freezes before the gate does, it is isolated and pulls a void regardless of the pressure above it. Section modulus decides the rigging, and the process will not rescue a bad one.
Mould strength and coating
The mould has to hold against the fill and then survive the metal. Printed sand is strong and consistent, but the coating still has to be right or the surface burns on and the casting picks up sand.
Distortion as it cools
A large thin-walled housing comes out of a restrained mould and moves as it cools. The printed mould's collapsibility helps; the rigging still has to let the part contract in the direction it wants to.
The riser stub and gate
Low pressure leaves one stub to cut rather than a feeder system, which is the advantage — but the cut has to be clean and below the finished surface, or it becomes a machining operation on a face that was supposed to be as-cast.
Low pressure castings we have poured
Switchgear housings, motor housings and enclosures — the family of parts the process exists for. Every one of them was cast into a printed sand mould, so every one of them could be a single part.
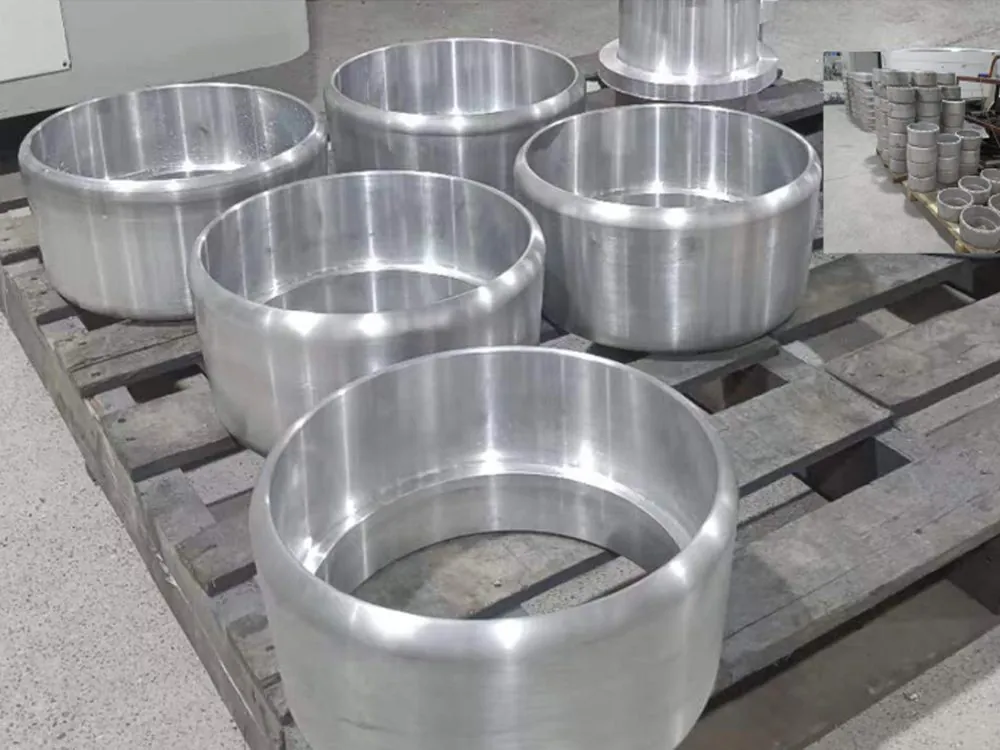
Corona shieldsAluminium, printed mould 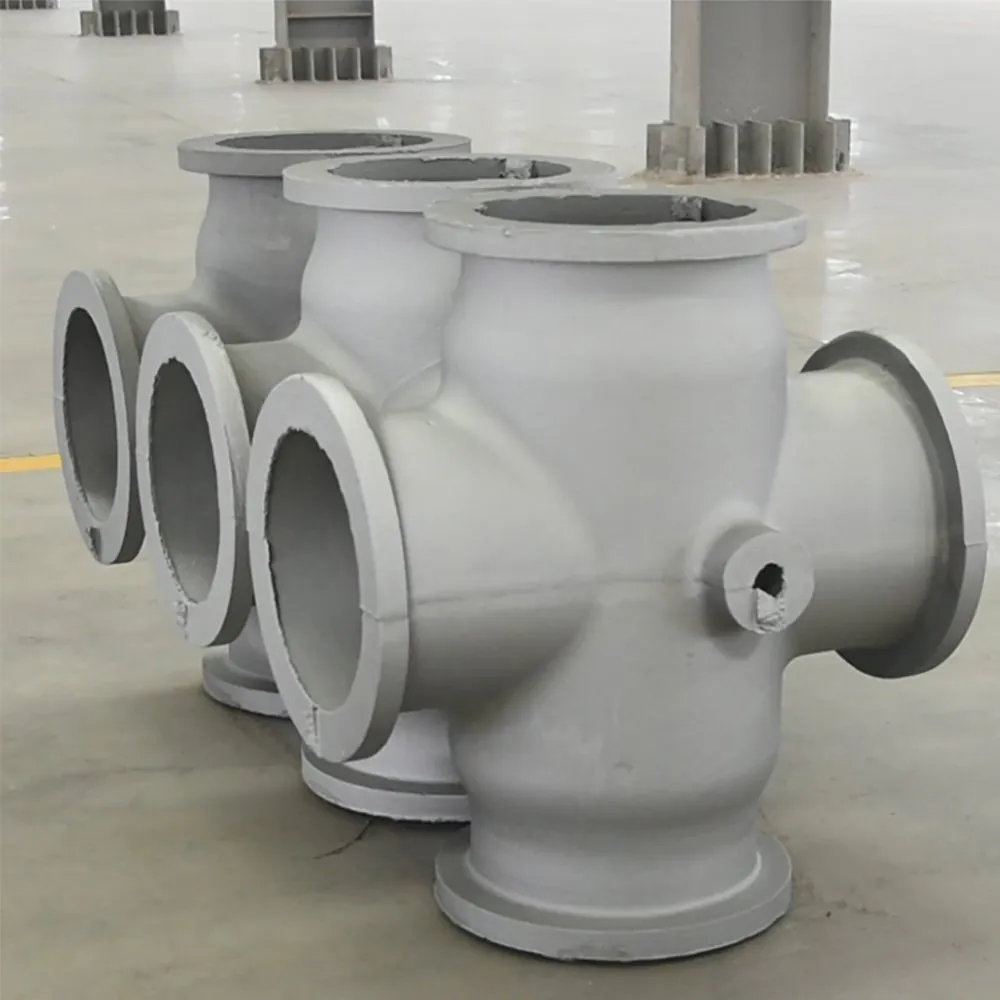
Ultra-high voltage GIS enclosureGas-tight, low pressure 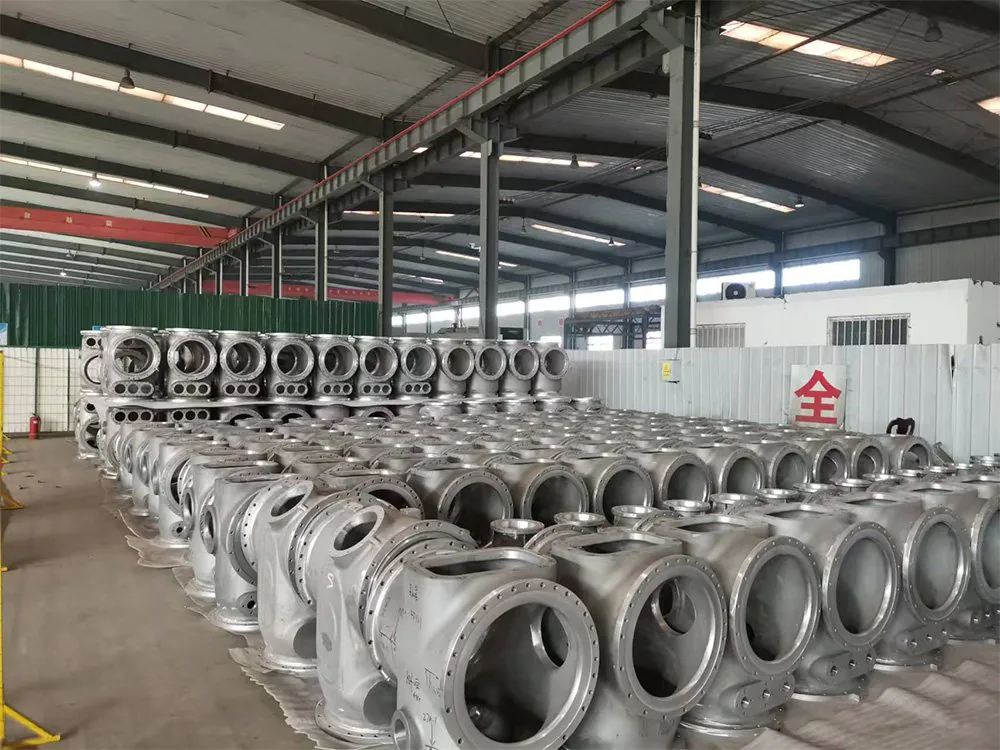
GIS enclosure batchProduction, not prototype 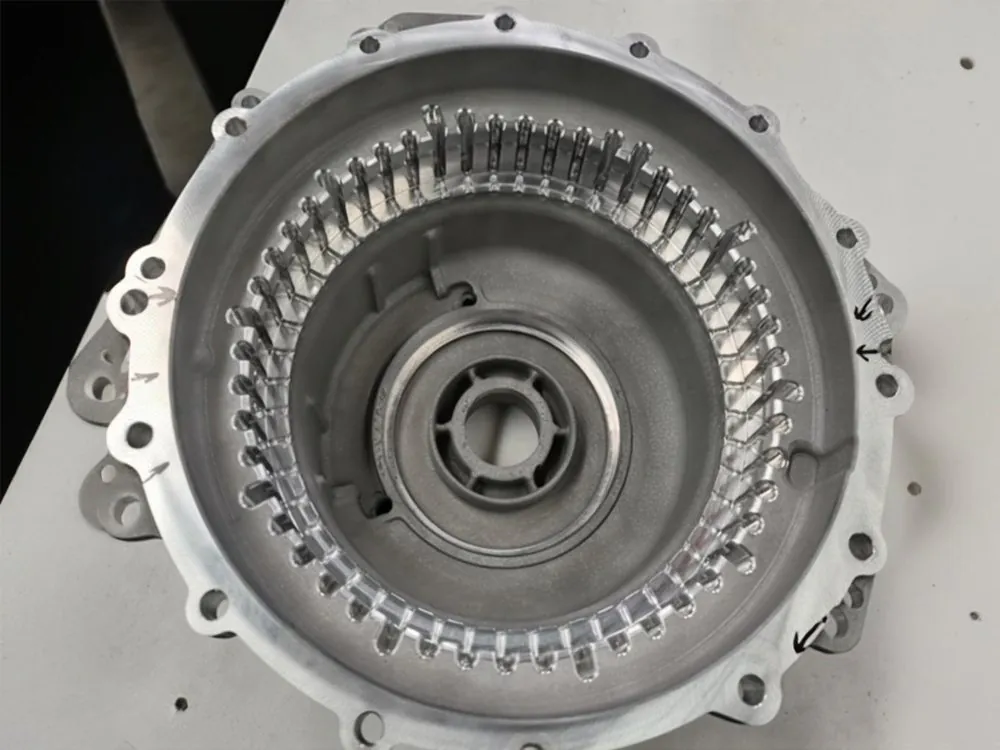
Motor housing in ZL101AMachined after casting 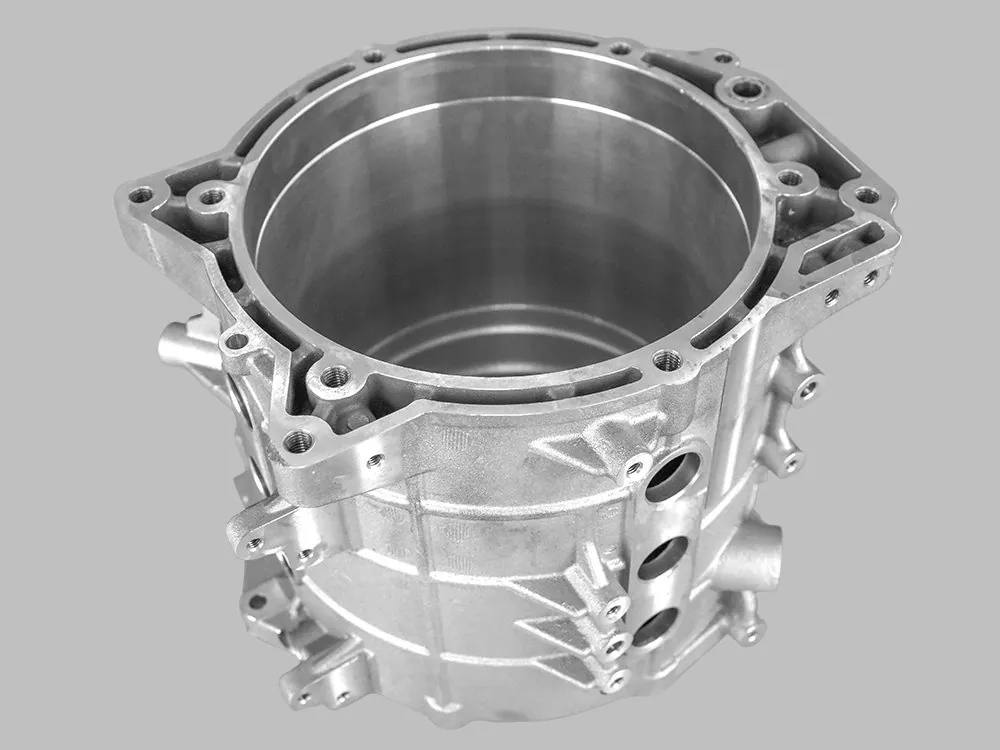
EV motor housingAluminium, thin-walled 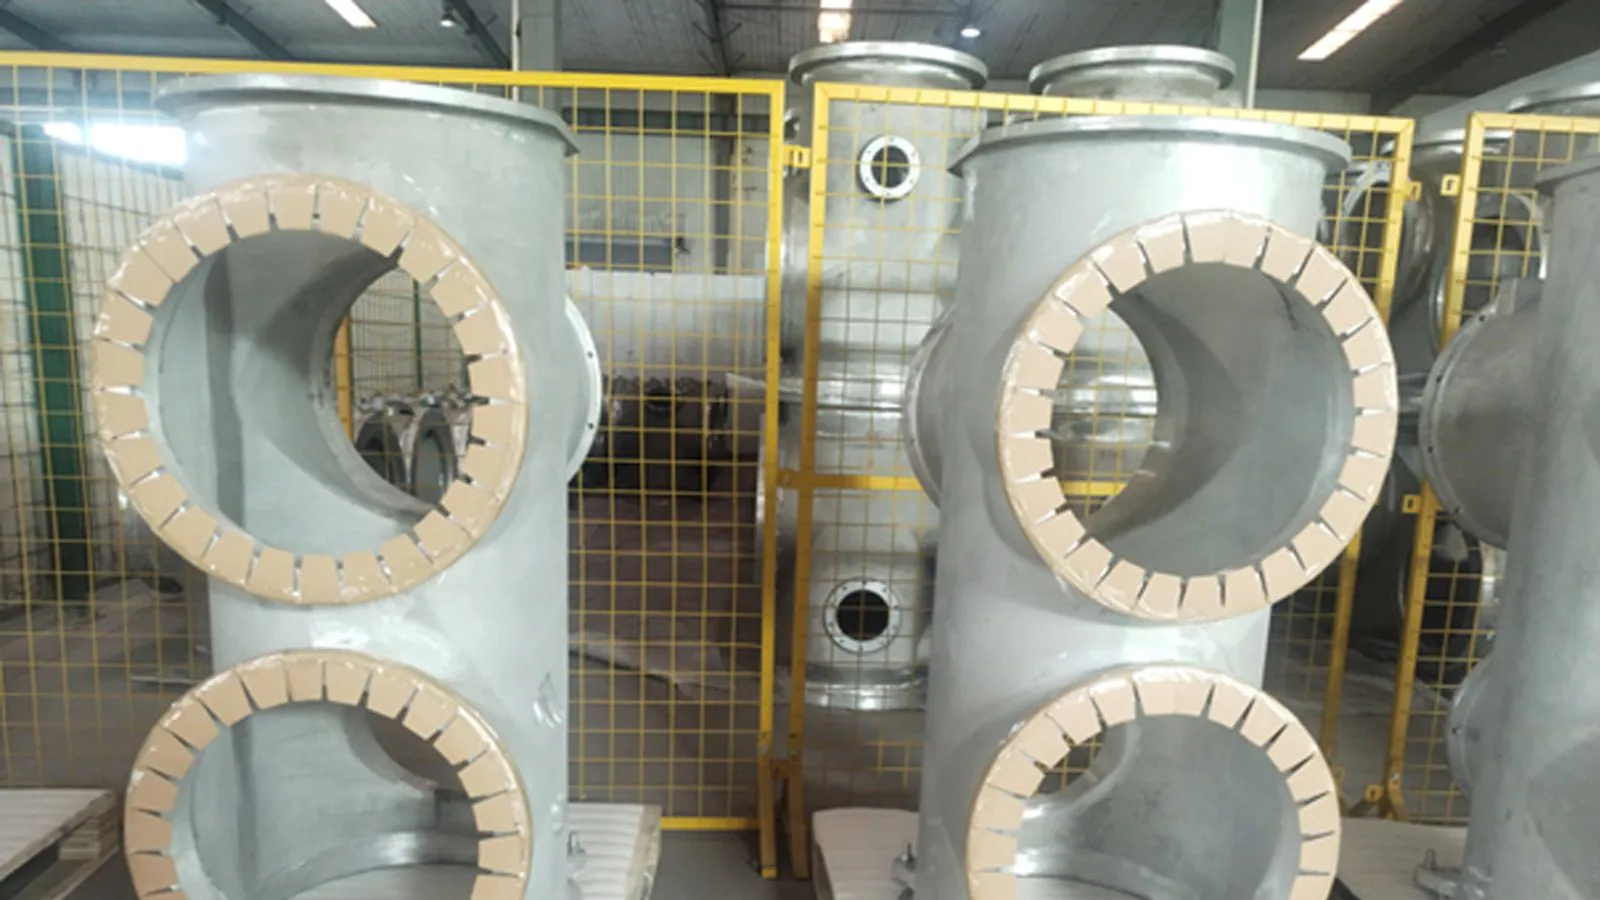
Switchgear housingsBatch, machined all over
Where low pressure pays off
The process wins wherever a part has to be dense and the quantity does not justify a steel die. In practice that is these:
Gas-insulated switchgear enclosures
The application this line was built around. Internal geometry that must hold insulating gas, wall sections that vary across the part, and volumes that never reach die-casting numbers.
Switchgear and control housings
Contact bases, cylinders, shielding and covers. Pressure-tight, fully machined, and often delivered as a small batch of several different parts together.
Motor and generator housings
Water-cooled jackets and motor end housings, in ZL101A and similar alloys. Thin walls with a cooling passage inside are exactly what the process feeds well.
EV and commercial vehicle parts
Water-cooled shells and housings for electrified drivetrains, where the part is new every model year and no die is worth cutting.
Pump and valve bodies
Aluminium bodies with an internal passage that has to be leak-tight. A gravity pour of the same geometry can weep; a low pressure pour usually does not.
Impellers and wheels
Parts where the vanes have to be sound through the section. The laminar fill and the pressure held during freezing both work in your favour.
What we do not do
Low pressure is a specific tool, and it is worth being precise about where it stops.
We do not high pressure die cast
High pressure die casting is the right answer above roughly 10,000 parts a year and it needs a hardened steel die. We do not run it. If that is your volume, a die caster will beat us on piece price and we will say so.
We do not run low pressure in steel
This line is an aluminium process. Low pressure steel exists in the industry but it is a different plant, a different refractory set and a different temperature regime, and we do not offer it.
We are not the fastest process
The cycle is slower than gravity die casting and much slower than high pressure die casting, because the metal is deliberately allowed to rise slowly. If cycle time is your binding constraint, this is the wrong process.
We do not quote a leak-tight part on geometry alone
Pressure-tightness depends on the rigging and the solidification order, not just the shape. Where a part has a real pressure or gas-retention duty we will confirm the process with a first casting rather than promising a number.
Choosing the right route for your part
If low pressure is not the answer, one of these is. Each runs the same printed-mould chain, so switching route does not cost you the lead time you were trying to save.
- Aluminium casting
The alloy family behind every part on this page, and the other processes it runs on.
- Precision investment casting
When the geometry is thin-walled and intricate rather than pressure-tight.
- Stainless steel casting
When the duty needs corrosion resistance and aluminium will not survive it.
- Sand mould and core printing
When you need the printed mould or core itself as a product, not the casting.
- Materials guide
To check the alloy against the rest of the range.
- الصب بالجاذبية
The sibling process — simpler parts where pressure-tightness is not the constraint.
- Bronze and brass casting
Copper alloys on the same printed-mould chain, for bearing and marine duty.
Not sure which one? Send the drawing and the duty, and let our application engineers make the call. We print the mould before you commit to tooling, so the route is tested rather than argued.
Low pressure casting questions
What is low pressure casting?
A casting process where a sealed furnace is pressurised with dry compressed air and the metal is pushed up a riser tube into a mould held above it. It fills slowly and laminar, and the riser keeps feeding the casting while it freezes.
Why choose low pressure over gravity casting?
Density and yield. The pressurised, laminar fill avoids the turbulence and oxide entrainment a gravity pour can create, and the riser feeds the shrinkage so the part comes out pressure-tight with very little feeder metal to remove.
Do you need a die for low pressure casting?
Conventionally yes, which is why it is usually a volume process. We cast into printed sand moulds instead, so there is no die and no pattern. That is what makes a single switchgear housing an economic order.
Which metals can be low pressure cast?
On our line, aluminium — ZL101A and similar. Low pressure steel and low pressure copper exist, but they are different plants and we do not offer them. For copper alloys and steel, see the links above.
How large a part can you cast this way?
The largest documented part on this page is a 2,250 × 420 mm conductor. Largest single aluminium pour is 1 t. If your part is outside that, send it and we will tell you honestly rather than quoting it.
How long does it take?
Every case documented above was delivered in 20 days as a small batch, from drawing to fully machined part. The mould-making cycle runs about 70% shorter than the traditional route because there is no pattern or die to make first.
Will my part be pressure-tight?
That is what the process is for, and it is why the switchgear and GIS work comes here. But pressure-tightness depends on the rigging and the solidification order for your specific geometry, so where a real pressure duty applies we confirm it with a first casting.
What tolerance and surface do you get?
CT8 to CT12 as cast to ISO 8062, with a printed mould surface around Ra 25µm against Ra 50µm or worse from a rammed sand mould. Anything tighter is machined, in the same chain, after stress relief.
Can you machine and inspect the castings?
Yes. CNC machining from 3-axis to 5-axis and nine inspection methods in house, including CMM and 3D scanning. Every part documented above was delivered fully machined against the drawing.
Is there a minimum order quantity?
One piece. There is no die and no pattern to amortise, so a single part is a legitimate order — and a batch of several different parts in one delivery is normal.
Send a drawing and we will say whether low pressure is right
Send the CAD file, the alloy if you have a callout, the pressure or gas-retention duty, and the quantity. Our application engineers will come back with the process, the rigging approach and a price — and if gravity casting or a die caster is the better answer for your part, that is what we will tell you.
Your file stays confidential. Nothing is subcontracted: the mould is printed, the metal is poured low pressure, and the casting is finished, machined and inspected in the same chain.